Best Reflective Alu Foil Factory Qualities That Guarantee Long-Lasting Thermal Performance
2026-11-18
A reflective aluminum foil can look nearly identical from one supplier to the next, but the qualities that keep it performing year after year are often invisible on day one. That is where factory-level decisions make the difference. Jinbo focuses on the production details behind long-lasting thermal performance, from alloy consistency to lamination control, so the foil does not just shine when installed—it keeps working through heat, humidity, and time. Here is what separates a dependable reflective foil from the rest.
Where Reflectivity Really Comes From in the Melt
A molten surface rarely owes its reflectivity to smoothness alone. In metallic melts the glare comes from conduction-band electrons that oscillate in phase with incoming light and reradiate it almost immediately, which is why a liquid metal can still look mirror-like even while flowing. That electronic response is tied to the metal's density of states and scattering rate, so composition and temperature shift both the brightness and the color of the reflection.
For oxide, slag, or polymer melts the mechanism is quieter. Reflection is mostly a dielectric effect at the interface, set by the difference in refractive index across the boundary. As the melt heats and its density changes, the polarizability per unit volume shifts, moving the reflected fraction up or down. Dissolved gases, bubbles, and thin oxide skins can either roughen the interface optically or add a partial reflective coating, altering what an instrument or eye actually sees.
Angle and wavelength matter just as much as chemistry. At grazing incidence even a slightly absorbing melt turns more mirror-like, while in the infrared the reflectivity of many melts tracks their electrical conductivity. Surface tension-driven ripples and thermal gradients blur the image without necessarily reducing total reflected energy, so the perception of shine in a melt is a mix of specular reflection, scatter, and emissivity.
How Gauge Control Keeps the Foil From Becoming a Weak Link
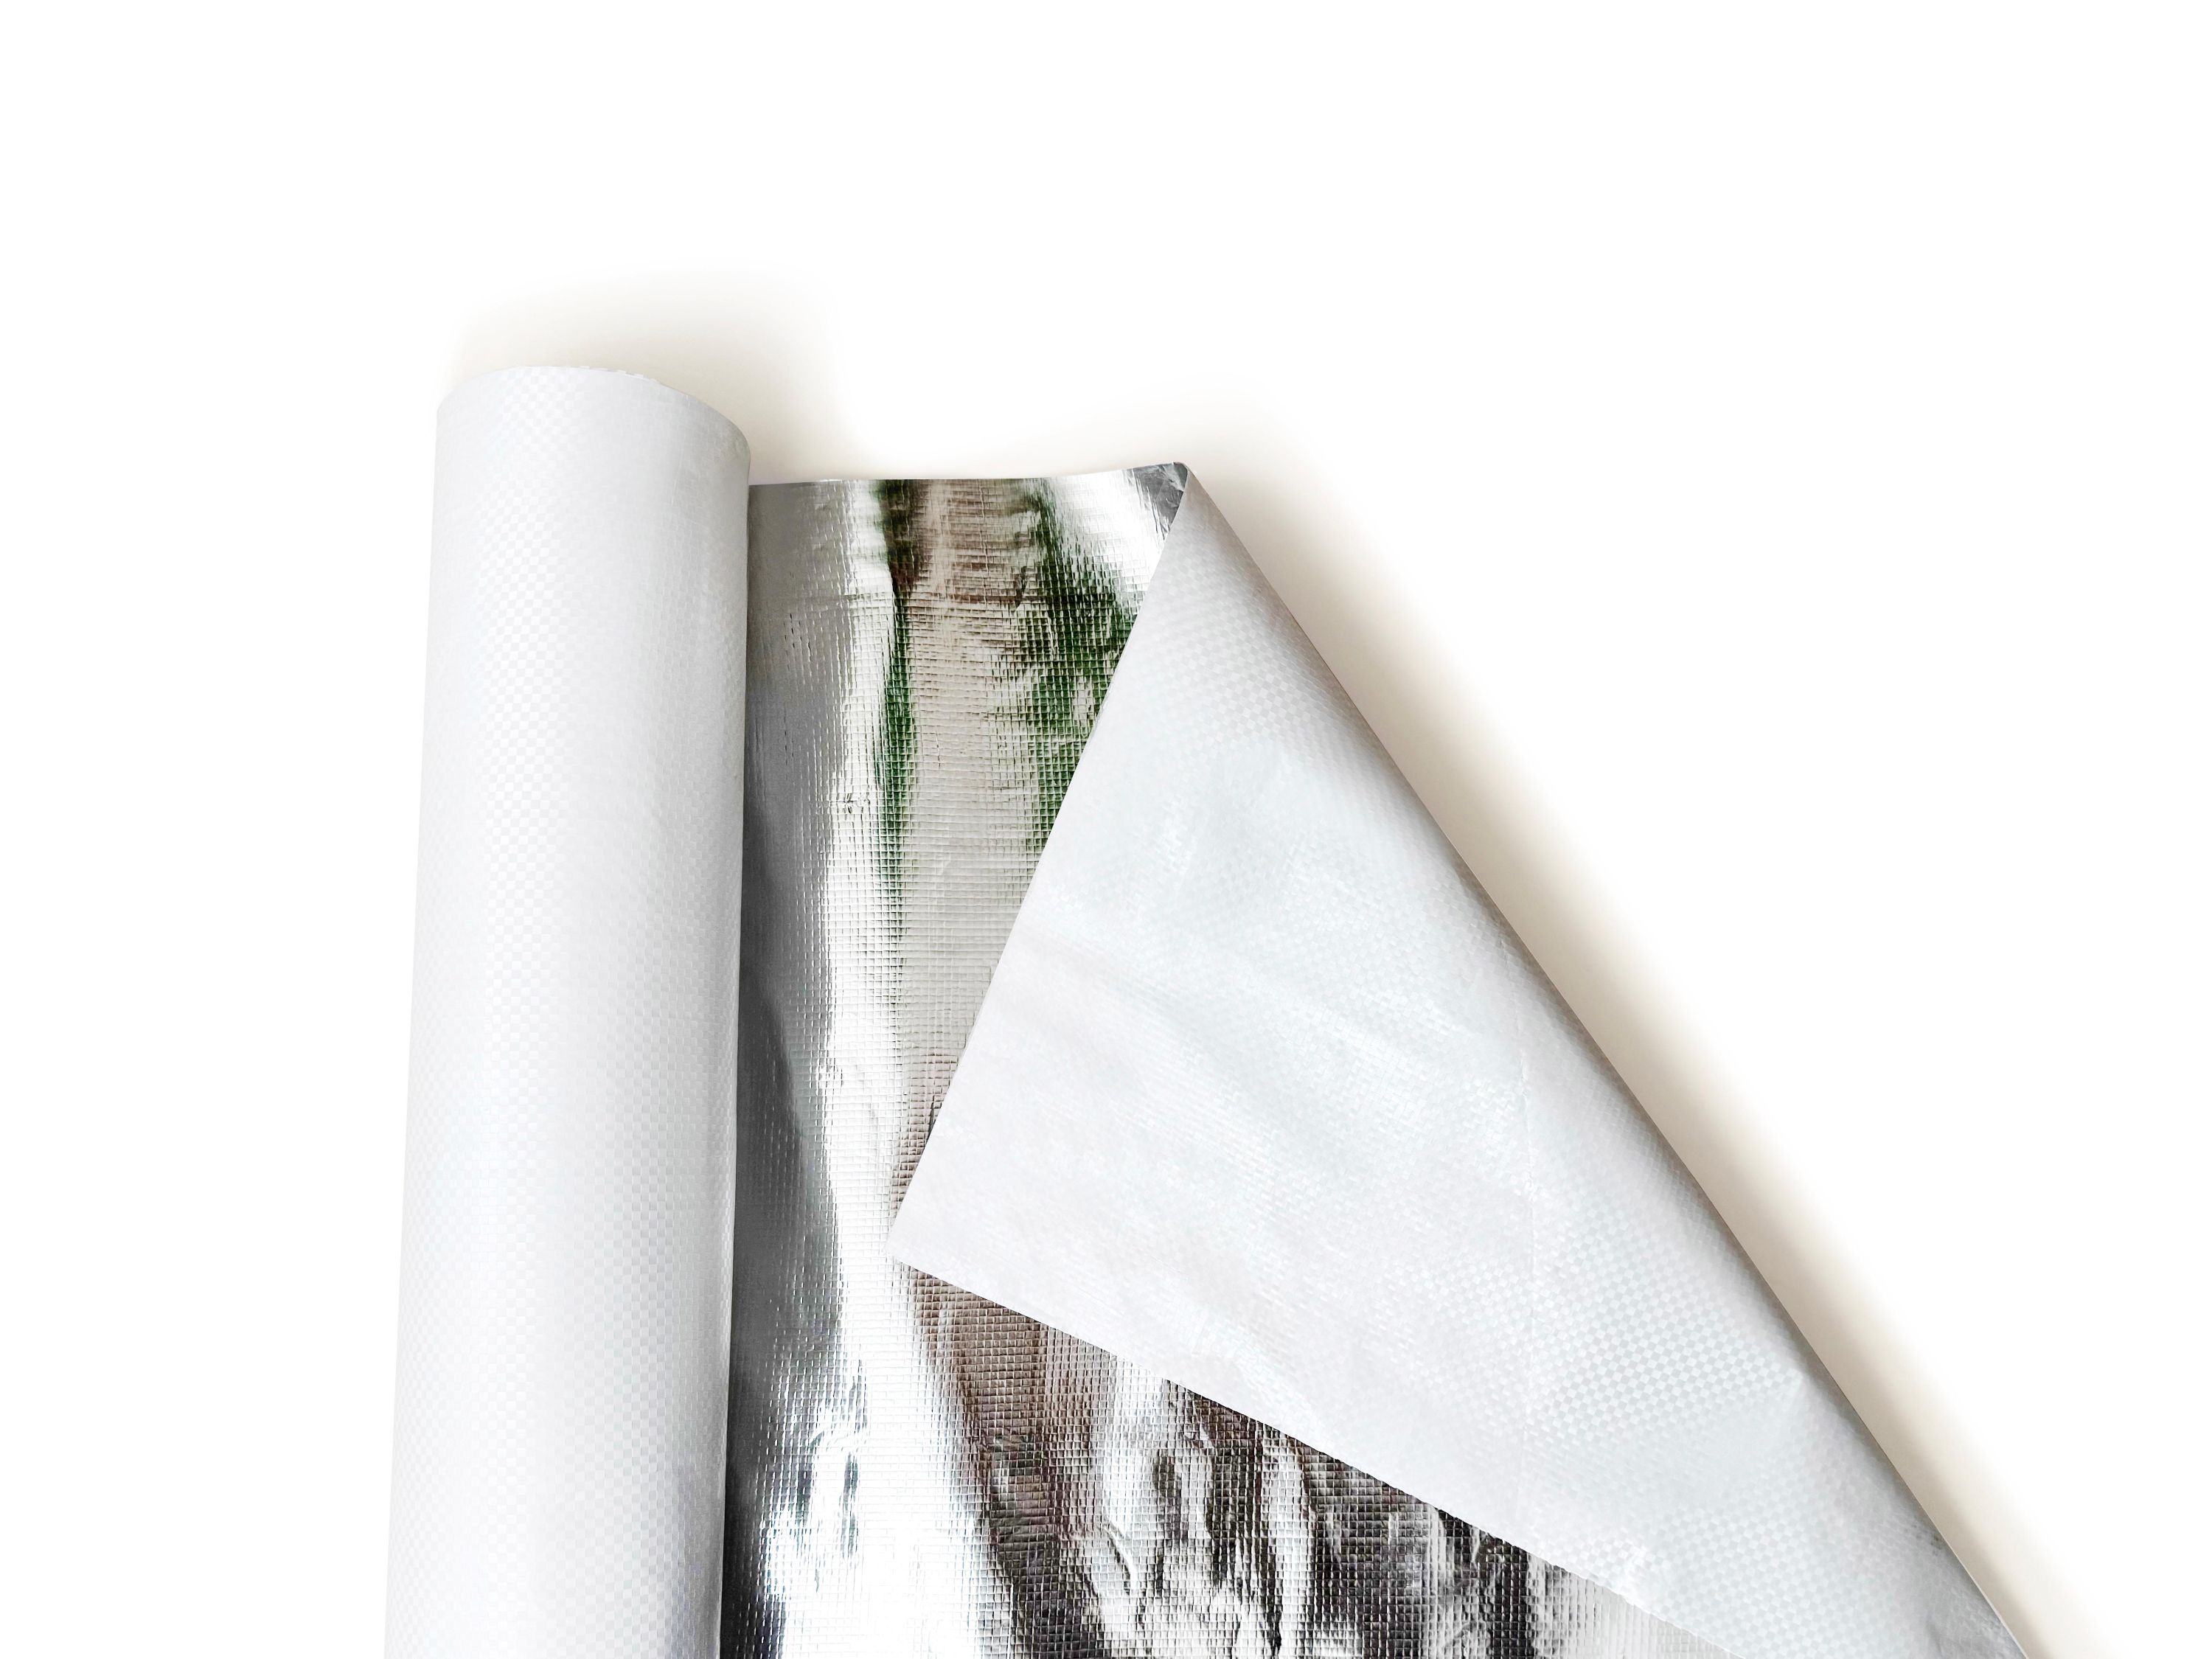
Foil might look uniform, but its thickness can drift during rolling, coating, or lamination. A few microns either way changes how it handles tension, heat, and puncture. Gauge control steps in here not as a post-process check, but as a live correction loop. Sensors placed close to the web read thickness in real time, and the system nudges roll pressure or line speed before a thin spot turns into a tear. That constant feedback is what keeps a single weak point from spreading across the whole roll.
What often gets overlooked is how small local variations interact with downstream converting. A pocket of slightly thinner foil might survive rewinding but fail under embossing, sealing jaws, or stretching. When gauge control holds tighter tolerances, the material behaves more predictably at every station. Operators spend less time chasing intermittent breaks, and the foil stops being the component everyone quietly distrusts. It becomes a stable input rather than a random source of downtime.
The most practical gauge systems don't just flag problems; they build a running map of thickness across the web. That map shows patterns, like edge thinning from a worn roll or a repeating dip from a tension spike. Once those patterns are visible, the fix is usually mechanical, not magical. Tightening gauge control often reveals that the foil itself was never the weak link. The real issue was a process drifting just enough to make normal foil look unreliable.
Why the Coating Has to Flex More Than the Metal
Steel and aluminium rarely sit still once they are in service. They bow under load, expand with heat, and snap back when stress eases. A coating bonded to that surface inherits every movement, but it cannot distribute strain the way the metal does through its thickness. Because the film is thin and locked at the interface, a modest bend in the substrate becomes a concentrated stretch at the coating's outer face. That alone forces the coating to accept more visible deformation than the part beneath it.
The difference turns harsher at edges, fasteners and welded joints. Movement concentrates in those spots, pulling the coating in several directions at once while the metal barely changes shape. If the coating's elongation falls short of that local strain, it splits long before the substrate reaches its own limit. Extra flexibility lets the film ride those stress concentrations instead of cracking along the line of least resistance.
Bend tests show the same story from a different angle. A coated panel is flexed until the first crack appears, and the coating usually fails while the metal still looks perfectly sound. Because the coating sits further from the neutral axis, its outer surface travels a longer arc during bending, and that extra distance becomes extra strain. Coatings that merely match the metal's flexibility tend to fail early. They need a reserve of elongation to survive repeated movement without opening a path for moisture or losing their grip on the surface.
Passing the Peel Test Before It Leaves the Loading Dock
Peel testing at the dock usually starts before the adhesive ever meets the substrate. Crews check surface temperature, wipe down edges, and pull a few inches of material by hand just to feel how evenly it releases. If the separation stutters or the backing tears, that hesitation is easier to correct while the batch is still on the floor than after it has been loaded onto a trailer.
The recorded values matter less than the pattern they leave behind. A steady number across the width of a roll tells a different story than a solid average with a soft left edge. Shift notes often call out slight changes in humidity, blade wear, or roll tension because those variables show up in the peel readings long before they cause a visible defect.
Once the last sample passes, the pallet gets checked against its paperwork and moved toward the dock door. The peel test is not there to create extra handling; it is there to catch the kind of failure that only appears after the product has traveled, sat in a warehouse, or been pulled apart by the end user.
Sealing Out Humidity at the Edges, Not Just the Center
Most moisture failures don't start under the middle of a film or coating. They start at the perimeter, where the seal meets a rough edge, a screw hole, a seam, or a change in material. If the center stays dry but the edges wick water, the barrier is already compromised. Edge sealing has to be treated as its own step, not an afterthought.
Corners and cut edges expose the substrate in ways a flat surface never does. A continuous center layer can look perfect while a thin gap at the edge pulls in humid air through capillary action. Using a flexible sealant or tape that overlaps the edge and bonds to the adjoining surface gives moisture fewer paths to follow. It also helps to knock down sharp edges before sealing, because a smooth transition holds a bead far better than a raw cut.
The difference shows up in high-humidity cycles. Sealed centers stay clear for a while, but edge failures appear as hazing, lifting, or slow staining that works inward. Checking the perimeter with a bright light, a fingernail, or a moisture meter catches those small breaches before they grow. Moisture control is won at the edges, where the seal is thinnest and the exposure is greatest.
When Factory Readings Predict What Happens After Installation
A factory reading is not a promise; it is a snapshot taken under controlled conditions that rarely survive first contact with a real site. Small differences in mounting torque, cable routing, ambient temperature, or even the way a panel is handled during shipping can nudge those numbers before the system is ever powered on. Treating the factory sheet as gospel often leads to unnecessary adjustments later, because the gap between bench conditions and installed reality is where many initial “faults” are born.
What makes the factory data useful is not its precision but its consistency. When a reading shifts after installation, the direction and size of that shift matter more than the absolute value. A uniform offset across channels usually points to installation environment or grounding differences, while one channel drifting away from its neighbors suggests a localized issue at a connector, sensor mount, or cable run.
The practical rule is simple: record the factory baseline, capture the post-install baseline under normal operating conditions, and only react to deviations between the two that exceed normal settling behavior. That approach turns the factory reading into a reference rather than a verdict, and keeps commissioning teams from chasing problems that exist only on paper.
FAQ
Reliability usually comes down to whether the plant controls the full rolling and coating process instead of buying semi-finished rolls from unknown sources. A dependable factory will share incoming aluminum grade certificates, surface roughness readings, and adhesion test results without being pushed. The ones that consistently perform in hot applications also run inline thickness gauges and reject coils that drift more than a few microns.
Look beyond the initial shine. Durable reflective foil depends on a clean substrate, a thin oxide-resistant treatment, and a polymer coating that is cured at the right temperature. If the surface feels chalky, leaves residue on a clean cloth, or shows fine cracks when bent, the top layer is likely too brittle. A lasting finish should survive a tape pull test and a repeated flex test without visible delamination.
Average thickness can hide dangerous weak spots. If a roll varies between two thicknesses across its width, the thinner lanes become radiant barriers that tear during installation and lose contact with the substrate. Factories that guarantee long-term thermal performance measure full-width profiles, not just edge samples, and they cut out the portions that fall outside tolerance.
The best plants keep bare aluminum exposure time short between rolling, cleaning, and coating. They also apply a conversion layer or primer that seals the metal surface against moisture and airborne sulfur compounds. Sensible packaging matters as well: vapor-barrier wrapping, dry storage, and edge protectors stop the kind of slow corrosion that starts before installation and shortens service life.
Adhesive failure is often mistaken for foil failure. If the adhesive softens at attic temperatures or becomes powdery after repeated hot-cold cycles, the reflective layer separates from the backing and the assembly loses its low-emittance performance. Strong factories use adhesives rated above the expected continuous service temperature and test bonded samples after thermal aging, not just fresh off the line.
A serious supplier should have data for total reflectivity, emittance, tensile strength, puncture resistance, and flame spread. More importantly, those results should come from independent laboratories and include the test method, date, and sample description. If a factory only offers a marketing sheet with glossy photos and no measured values, that is usually a sign the process is not tightly controlled.
Final inspection only catches defects before shipping. A well-run factory uses process control points at each stage: incoming alloy checks, rolling tension monitoring, coating weight verification, and air-gap measurement for lamination. Operators record the data in real time and can trace every finished roll back to a specific aluminum coil and production shift. That traceability is what turns a good batch into a consistently reliable product.
Yes, but only if the factory treats slitting and laminating as part of the thermal design, not as afterthoughts. Slitting must produce clean edges without burrs or micro-cracks that invite corrosion. Multilayer builds need compatible adhesives and controlled tension so the reflective surface stays flat and continuous. When these steps are properly managed, custom formats can match or even exceed the performance of standard rolls.
Conclusion
Reflective aluminum foil rarely fails because of a single dramatic flaw; it fails when small inconsistencies in the melt, rolling, and coating process line up in the wrong way. The base reflectivity is set long before lamination, in the melting and casting stage, where oxide control and alloy cleanliness determine whether the surface will hold a mirror-like finish or drift into a hazy, heat-absorbing gray. After that, gauge control becomes the quiet variable. A foil that runs slightly thin in one area may still look uniform on the roll, but under tension, thermal cycling, or contact with insulation it becomes the point where tearing starts. Coatings have to be more forgiving than the metal itself, stretching and flexing through bends without cracking away from the reflective layer.
The qualities that matter most are verified before shipment rather than assumed from material specifications. A peel test at the loading dock tells more about long-term adhesion than any visual check because it exposes whether the coating is bonded or merely resting on the surface. Edge sealing receives the same scrutiny; humidity typically enters at the cut edges first, so a factory that only protects the center of the sheet is leaving the most vulnerable path open. What separates a dependable supplier is less about glossy brochures and more about the data collected on the line. When factory readings for reflectance, thickness, adhesion, and edge moisture resistance are tracked together, they offer a realistic preview of how the foil will hold up after installation, not just how it performs on a sample card.
Contact Us
Contact Person: Miranda
Email: [email protected]
Tel/WhatsApp: +8615231299719
Website: https://www.ihousewrap.com/