CNC Press Brake Manufacturer Guide to Boosting Fabrication Efficiency
2026-09-21
Ask any fabrication shop owner what keeps them up at night, and 'press brake bottlenecks' will likely top the list. But what if the real problem isn't your operators, but the machine itself? In this guide, we break down how switching to the right CNC press brake—like those from HUNSONE—can slash setup time, reduce scrap, and unlock throughput you didn't think was possible. Don't let outdated bending tech cap your shop's potential.
Tooling decisions that quietly eat your profit margins
Most shops don't notice the slow bleed until month-end reports show tooling line items that look harmless on their own but stack into a five-figure annual leak. That extra monitoring dashboard nobody checks, the project management add-on purchased for a team of three, the design tool with seats still assigned to former employees. Each one was justified at the time as a small convenience, yet collectively they behave like a subscription tax on your gross margin.
Then there's the less visible cost: switching and maintenance. Every new internal tool carries a learning curve, integration glue code, and someone's Friday afternoon spent patching it when an API changes. These hours rarely show up under "tooling" on the P&L. They hide inside payroll, delayed releases, and the occasional firefight when an unsupported plugin breaks a build. Replacing a $50/month tool with a slightly cheaper one may save the invoice, but if it costs a developer a day to migrate, the profit hit was already taken.
A practical fix is to treat tooling like inventory: review it quarterly, attach an owner to each subscription, and retire anything that hasn't been opened in 90 days. The goal isn't to strip the stack bare—some tools genuinely save hours—but to force every recurring cost to prove it still earns its place against the margin it quietly consumes.
Why your press brake’s idle time isn’t what you think
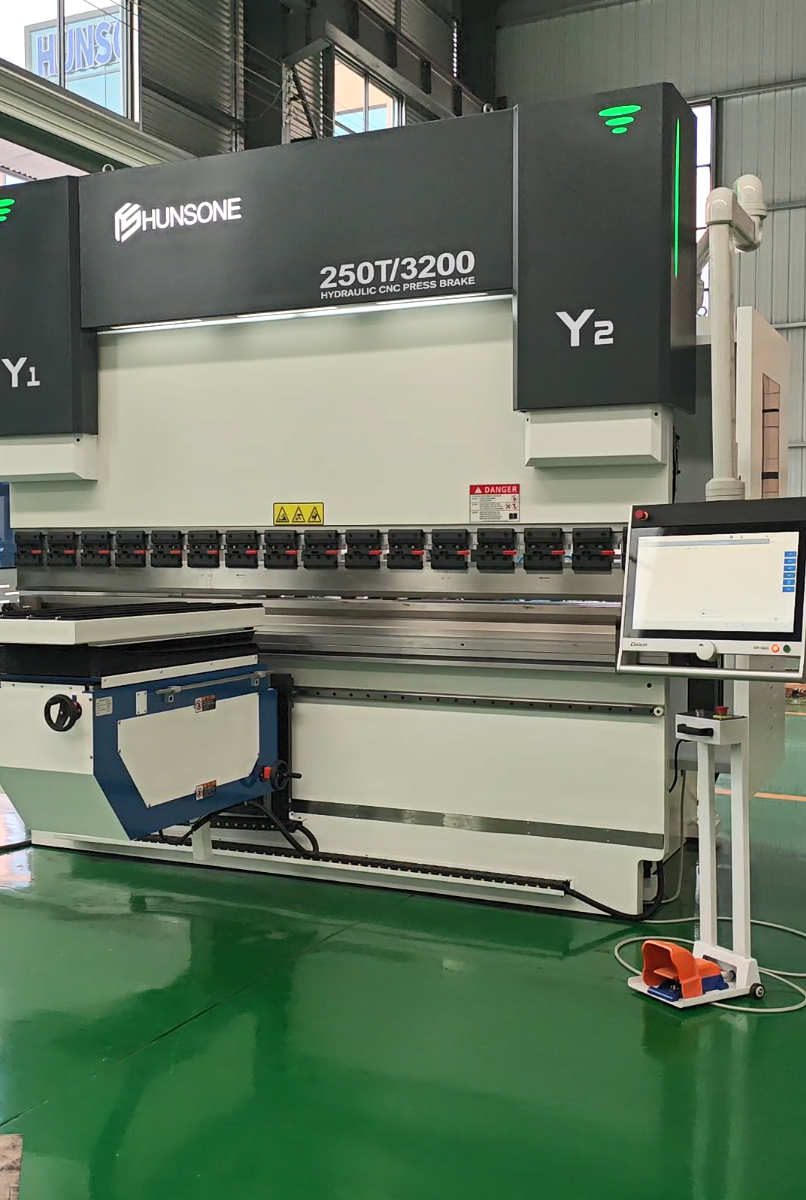
Many shops log idle time only when the ram stops moving. But on a press brake, the backgauge keeps hunting for position, the pump idles under load, and the operator may be fetching a different punch or checking a drawing. Those minutes don't show up as "idle" on most controllers, yet they are exactly when the machine isn't bending metal.
Even when the control says the brake is "in cycle," a pause between hits for part flipping or re-clamping gets averaged into cycle time, not idle. That skews the real picture. If you want a true idle number, track the time between the last bend of one part and the first bend of the next, including tool changes and first-article checks. Only then does the idle figure start to match what the floor actually feels like.
Bend simulation mistakes that snowball on the floor
A small oversight in bend simulation rarely stays small once the part leaves the screen. Take springback, for instance. If the software doesn't capture the material's true hardening curve, the predicted bend angle might be off by a degree or two. That's easy to dismiss in the model, but when the actual sheet metal comes off the press and sits on the shop floor, those couple of degrees compound across a long flange. Suddenly the part rocks on a flat surface, and the assembly team wonders why nothing lines up.
Another classic slip is meshing the bend region too coarsely. The solver smooths over stress concentrations, so the simulation says the bend is safe. In reality, the sharp radius cracks or thins out during forming, and that flaw travels downstream. By the time the parts are laid out on the floor for inspection or welding, the accumulated distortion from three or four 'negligible' simulation errors turns a flat panel into a wobbly mess. The fix isn't fancy—just refine the mesh locally and double-check the friction and tooling offsets—but ignoring those details is exactly how small mistakes snowball into floor-level headaches.
Offline programming without the usability nightmares
Most offline coding tools feel like a step back in time—clunky interfaces, missing autocomplete, and documentation that vanishes the moment your Wi-Fi drops. Developers have learned to dread long flights, remote cabins, or even just a shaky home connection because the moment the signal fades, their carefully tuned workflow falls apart. The pain isn’t just losing access to Stack Overflow; it’s the tiny, constant frictions: a package manager that refuses to work offline, an editor that suddenly forgets every function signature, and a debugger that demands a server sync before letting you inspect a local variable.
This experience flips that script by treating connectivity as an optional layer, not a lifeline. Language servers, linting rules, and type definitions are bundled directly into the environment, so you get smart completions and inline error checking whether you’re on a submarine or in a Faraday cage. Dependency graphs are snapshotted ahead of time, letting you install, update, and roll back libraries entirely from local storage. Even reference material lives inside the tool—no more dead links when you hit F1—because everything from API docs to migration guides is pre-fetched and indexed for instant search.
What really makes it feel different is how the software respects your attention rather than punishing you for disconnecting. Transitions between online and offline states happen silently; you won’t see a modal screaming “No Internet Connection” or a spinner that never ends. Version conflicts are handled through deterministic local resolution, not a frantic call to a registry. The result is an environment where offline work isn’t a degraded mode you tolerate, but a fully capable state you might actually prefer—quiet, fast, and entirely under your control.
The maintenance schedule your machine actually needs
Most maintenance charts are built for ideal conditions that rarely exist on a real job site. Dust, temperature swings, moisture, and how hard you push the equipment all change how quickly parts wear. Instead of blindly following a generic calendar, start by observing your machine's daily behavior. Listen for changes in sound, watch for small leaks or vibrations, and note how often you have to make minor adjustments. These signals often reveal a more accurate rhythm than any manual ever could.
Build a schedule around the hours you actually log, not just the date on the wall. If you run two shifts through abrasive material, a monthly filter swap might be far too late. Keep a simple written log near the machine—nothing fancy, just dates, hours, and what you did. After a few weeks, patterns emerge: maybe the hydraulic fluid darkens after 60 hours instead of the recommended 100, or the air filter clogs faster when you work near gravel. Adjust your intervals to match that reality.
Don't be afraid to shorten intervals for high-stress components while extending others that stay clean and cool. A one-size-fits-all plan often wastes money on premature replacements or, worse, lets a critical part fail. Talk with your operator about what they feel and hear—they know the machine's personality better than any spec sheet. The right schedule is the one that prevents downtime without over-servicing, and that only comes from paying attention to your specific operating environment.
Operator know-how that no manual captures
Every plant has a handful of people who can hear a bearing starting to fail before the vibration sensor blinks. They adjust feed rates by the way the machine breathes, not by the numbers on the screen. That kind of operator know-how lives in fingertips and ears, not in standard operating procedures.
New hires often shadow these veterans and learn odd rituals: a tap on the hydraulic valve, a pause at a certain temperature, a subtle offset that keeps a tool from chattering. None of it appears in the manual, because it was never engineered—it was earned through ruined batches and near misses.
Capturing that knowledge means asking better questions during shift handovers and filming real runs, not just documenting ideal conditions. The moment someone retires, the unofficial tricks leave with them unless they are passed on deliberately.
FAQ
It usually comes down to how the ram, backgauge, and control system share data. A machine with a fast but sloppy backgauge can create more rework than it saves. Look for closed-loop positioning on every axis, a crowning system that reacts to load in real time, and a control that lets operators pull up proven bend programs instead of re-teaching each setup.
In many job shops, tooling changes eat 20 to 40 minutes per job once you include searching, cleaning, and recalibrating. Manufacturers that standardize on a common tool height, offer quick-change clamping, and provide clearly labeled storage carts help cut that to under five minutes. The goal is to make the next setup predictable, not a scavenger hunt.
Yes, if the shop handles more than a handful of part numbers each week. Offline programming lets someone prepare bend sequences and simulate collisions without tying up the machine. The real payoff shows up when the operator loads a program and the backgauge and tools are already where the software expected them to be.
Under load, every press brake frame flexes a little. If that flex varies with material thickness and bend length, the operator has to compensate angle by angle, which slows everything down. A stiffer frame paired with an active crowning table keeps the bend angle consistent across the full stroke, so fewer test bends and shims are needed.
The boring stuff matters most: checking hydraulic oil cleanliness, greasing guide rails on schedule, and keeping the backgauge ball screws free of debris. Many failures trace back to contaminated oil or skipped lubrication. A good manufacturer will include sensor feedback for filter life and tool clamp pressure, but that only helps if someone actually reads the alerts.
It usually makes sense when part weights exceed what one operator can handle safely for a full shift, or when the same part family runs repeatedly. A robot adds value by keeping the machine bending during breaks and by removing variability in part placement. For high-mix, one-off work, a well-trained operator with a good backgauge often beats a robot on cost per part.
Track three numbers: setup time per job, first-part acceptance rate, and actual bending hours per week. Cycle-time improvements look nice in a demo, but if setup time stays flat and first parts need rework, overall output won't move much. Those three metrics expose whether the machine, tooling, and programming workflow are aligned.
For thinner materials and shorter runs, yes, because they only consume energy during the bending motion and return to idle without pumping oil. They also eliminate hydraulic warm-up time in cold shops. However, for very thick plate or heavy continuous production, a well-designed hydraulic system with variable pumps can still hold its own. The efficiency gain depends more on the control logic and operator habits than on the motor type alone.
Conclusion
Most fabrication shops look for efficiency gains in cycle time, but the real drain often hides in tooling choices that seem harmless at the quote stage. A punch and die set that requires extra shimming or forces the operator to rework bend allowances quietly turns a two-minute setup into a twenty-minute correction loop. That idle time on the press brake is rarely true waiting; it's usually spent chasing tooling, double-checking programs, or re-cutting parts because a bend simulation ignored grain direction, springback, or actual material thickness. Offline programming helps only when the software gets out of the way—if the interface demands constant workarounds, operators abandon it and go back to trial bends at the machine.
A smarter maintenance schedule targets what actually drifts: backgauge repeatability, hydraulic temperature stability, and clamp wear, not just the hours listed in a generic manual. Operators who run these brakes daily carry knowledge that no documentation captures—how a specific batch of stainless reacts to the ram, when a slight noise means the tooling has shifted, or which bends need extra dwell. A manufacturer guide that treats this tacit know-how as part of the system, turning it into better defaults and clearer training, removes the small frictions that accumulate into missed deadlines and lost margin. Efficiency comes from closing those quiet gaps, not from asking the machine to cycle faster.
Contact Us
Contact Person: James Chen
Email: [email protected]
Tel/WhatsApp: 86 13770803946
Website: https://www.hunsone.com/