Export Cooling and Automation Systems with Greater Efficiency and Reliability
2026-11-21
Every shipment that loses temperature stability or stumbles on automation costs more than money—it costs reputation. Yet many export setups still run on patchwork fixes and hope. This blog unpacks how smarter cooling and automation architectures deliver the consistency that global customers notice. Along the way, we’ll show why THINKING-LONG approaches system design as a whole, not as a collection of components.
Cooling Performance That Survives the Trip and the Climate
Heat, dust, and long stretches of rough road have a way of exposing weak cooling. The unit doesn't just survive those conditions; it keeps the inside temperature calm while the outside panel sits in direct sun. The compressor works in short, smart bursts instead of a constant roar, so the cold holds without draining the vehicle battery.
On a trip that swings from dry desert passes to damp coastal air, the seals and airflow matter just as much as the compressor. The lid stays firm after hours of vibration, and the intake side is positioned to avoid the worst dust pull. You can hear it, but only as a low, steady breath rather than a struggle.
The result is a cold space that recovers quickly after every stop. Ice keeps its edges, drinks stay cold near the top, and food at the bottom doesn't turn into a block. That's what makes the cooling useful after the third or fourth day on the road.
Automation Logic Adapted to Regional Power and Operator Habits
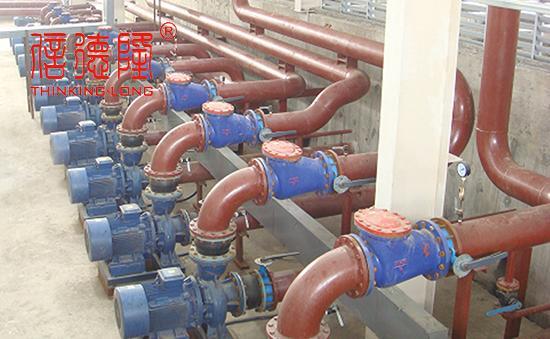
Regional grid codes rarely align perfectly, and operators in different markets have developed their own ways of working under local constraints. Rather than forcing a universal sequence on every site, the automation layer here is tuned to respect those habits. For instance, in areas where manual confirmation before breaker closure is standard practice, the logic waits for that local signal instead of assuming a fully hands-off flow. Elsewhere, where operators expect rapid auto-reclose after transient faults, the timing windows and dead-time settings are adjusted to match familiar operational rhythms, not some abstract vendor default.
This adaptation also extends to how power quality events are handled. Some regions prioritize voltage stability during peak load, while others focus on frequency response due to weaker interconnections. The automation rules therefore shift their trigger thresholds and response priorities accordingly. A sag that would initiate load shedding in one grid might only trigger an alarm in another, because the local operators have learned over years what works for their load mix and protection coordination. The logic is not a fixed recipe but a set of modular behaviors that can be weighted differently per deployment.
The result is a system that feels familiar to the people who run it, reducing the friction of adoption. Instead of retraining operators to fit the software, the software bends to the operating culture. That might mean preserving a particular step in a switching procedure, or keeping a legacy interlock that other regions have abandoned. By treating regional habits as inputs rather than obstacles, the automation becomes less visible as a foreign tool and more like a natural extension of existing practice.
Precise Temperature Control With Lower Compressor Duty
Fixed-speed compressors rarely match the way a room actually loses or gains heat. They switch on, push the space past the setpoint, then shut down and wait for the thermostat to fall behind again. Lowering compressor duty changes the rhythm. The unit still cycles, but each running period is longer, softer, and matched more closely to the real cooling load, so the temperature graph flattens out instead of forming sawtooth peaks and dips.
That gentler rhythm usually comes from a controller that samples the return air at short intervals and trims the duty ratio rather than waiting for a large error. The coil has time to settle into a stable operating range, which also keeps latent heat removal more consistent. You get less swing in both temperature and humidity, especially during mild weather when a full-power compressor would be oversized for the job.
The practical benefits show up quickly. Startup stress on the motor and refrigerant lines drops, the background hum fades, and the system uses less energy on pull-down spikes. It is a control strategy that suits bedrooms, wine cabinets, climate-controlled storage, and anywhere else where a steady baseline matters more than peak cooling speed.
Fault Warnings That Arrive Before Production Stops
When a production line halts without warning, the cost is never just the downtime itself. The real damage hides in the scramble that follows: rushed diagnostics, half-tested fixes, and operators second-guessing what they saw on the control panel. A fault warning that arrives days or even hours before the stop changes that entire dynamic. It gives maintenance teams a window to observe the drift, check the usual suspects, and decide whether a brief intervention now is cheaper than a full stop later.
These early warnings rarely look dramatic. A slight rise in motor current, a vibration signature that edges outside its normal band, or a temperature trend that no longer flattens out after warm-up. None of these shout “failure incoming,” yet each is a quiet signal that the machine’s baseline has shifted. The value lies in learning what normal looks like for a specific line, not a generic one. Two identical pumps in the same plant can have different healthy patterns, and warning logic that treats them the same will cry wolf too often or stay silent too long.
The practical goal is not to predict every possible failure, but to make the first sign of trouble visible early enough for a considered response. That might mean rescheduling a batch, swapping in a spare part during a planned gap, or simply watching one more shift before deciding. In most plants, that kind of breathing room transforms maintenance from firefighting into something closer to routine adjustment.
Modular Builds That Reduce Installation Time at Destination
A modular approach shifts most of the finish work into a factory, so what arrives on site is closer to a completed structure than a pile of materials. Panels or room-sized units show up with wiring pulled, plumbing tested, and trim already in place. On the destination side, the crew spends less time cutting, fitting, and waiting for inspections because those steps were closed out before shipping.
That compression changes the daily rhythm of a job site. Instead of sequencing framing, rough-in, drywall, and finishes over several weeks, the field team can move straight to setting modules and making the final connections. A smaller crew with a crane can often complete the main structure in one or two shifts, which keeps weather delays, material theft, and rework from eating into the schedule.
There is also a repeatability advantage. Once a module design has been built a few times, the factory line and the installation crew both settle into a faster pattern. Connection details become familiar, packing loads are optimized, and even first-time site supervisors can work from a proven sequence rather than solving every condition on the fly.
Lower Energy Use at Partial Load Without Sacrificing Throughput
Most machines take a real efficiency hit the moment they step away from full load. This one is tuned to behave differently. Instead of wasting energy through throttling or frequent start-stop cycles, it adjusts output to match demand while keeping the core process moving at the same pace. The result is a flatter efficiency curve across the operating range, not just a strong number at one point.
That matters in practice because real production rarely sits at a single load. Shift changes, material variations, and downstream bottlenecks all push equipment into partial-load territory. By focusing on how the system responds in that middle ground, the design trims power draw without adding cycle time. Operators can run smaller batches or uneven schedules without watching energy per unit climb.
The payoff shows up in everyday operation. Lower heat generation, less wear on moving parts, and steadier power demand all stem from the same underlying control strategy. Throughput stays predictable because the equipment is not pausing or compensating with extra passes; it simply works closer to the actual requirement, and the meter reflects that discipline.
FAQ
Reliability mostly comes from using components that tolerate supply chain delays, voltage fluctuations, and rough handling. I'd look for sealed compressors, coated control boards, and firmware that can self-diagnose rather than fail silently.
Automation cuts costs by letting the system adjust fan speed, defrost cycles, and compressor staging based on actual load instead of a fixed schedule. That avoids energy waste and keeps components from wearing out early, which matters more when replacement parts are far away.
Fumigated crates, moisture barriers, and shock-absorbing mounts usually matter more than extra branding. If the unit arrives with corroded terminals or a cracked manifold, no amount of documentation fixes the first impression.
Yes, if the control logic handles 50/60 Hz, wide voltage tolerances, and high ambient conditions. The more important part is letting local technicians change setpoints without needing proprietary software.
Design around modular parts and common fittings so a local distributor can stock fewer SKUs. Remote diagnostics also help by identifying the actual fault before a technician is dispatched.
Manuals and wiring diagrams are sometimes treated as an afterthought, but overseas installers rely on them more heavily. Clear torque specs, refrigerant charge tables, and fault-code explanations prevent unnecessary warranty claims.
Efficiency is often tied to import duties or incentive programs in many markets, so a system that exceeds MEPS can enter more easily. It also lowers total cost of ownership, which resonates with buyers planning a 10-year lifecycle.
Run the unit in an environmental chamber that cycles between high heat, humidity, and salt mist while the controller is actively managing load. That catches sensor drift and condensation issues that won't show up in a dry factory test.
Conclusion
Export-focused cooling and automation equipment has to earn its place long before it reaches the customer. The real test is not in a controlled demo but on a truck crossing equatorial humidity, through ports with unstable handling, and into facilities where voltage sags or phase balance varies from one shift to the next. Refrigeration circuits that hold their charge, valves that do not drift after rough transit, and controllers that accept local grounding practices make the difference between a smooth startup and a callback. In many regions, operators expect familiar sequences and manual override points, so the automation layer needs to adapt without forcing a retraining burden. A rugged cooling package paired with tolerant control logic usually outperforms a more sensitive system that looks impressive on paper.
The efficiency side matters just as much once the unit is running. Rather than pushing compressors hard to chase a single setpoint, smarter staging and tighter superheat control keep temperatures steady while reducing starts and runtime. That lowers energy use at part load without slowing production, which is critical where power costs are unpredictable. Fault warnings tied to actual performance trends, not fixed timers, can reach maintenance staff early enough to clean a condenser or check a fan before a line stops. Modular frame and piping layouts also shorten installation at destination, since pre-wired sections and labeled connections reduce site labor and miswiring. Together, these details create equipment that survives the trip, fits local operations, and keeps running with fewer interruptions.
Contact Us
Contact Person: Qian Xijun
Email: [email protected]
Tel/WhatsApp: 8613961736750
Website: https://www.thinkinglong.com/