Press Brake Machine Company Questions You Should Ask Before Buying
2026-09-17
Most press brake buyers obsess over tonnage and price, yet the questions that truly separate a smart purchase from a costly mistake rarely appear on a spec sheet. Before you commit, ask the uncomfortable ones—about support, tooling, and real-world accuracy. HUNSONE's team has fielded these conversations for years, and the answers often surprise even seasoned shop owners. Here’s what to ask before signing.
How Their Service Team Reacts When Your Machine Goes Down
A machine failure rarely happens at a convenient moment. Their service team doesn't wait for a ticket to sit in a queue—once the call or alert lands, a dedicated engineer familiar with your equipment history picks it up. You won't get bounced between departments; the person who answers knows what you're running and can often walk you through immediate containment steps while they pull up diagnostics.
From there, the response shifts to faster resolution rather than just remote troubleshooting. If the issue looks mechanical or electrical, a local field tech is dispatched with the likely parts already loaded, not sent out empty-handed to "take a look first." They'll coordinate with your maintenance lead on site access and lockout procedures, so downtime doesn't get extended by back-and-forth scheduling.
The follow-up matters just as much. After the machine is back online, you receive a short summary of what failed, what was replaced, and what might prevent a repeat—not a 20-page report buried in jargon. If the same fault recurs within a short window, the team treats it as an open case and escalates internally instead of making you start over.
What Past Buyers Say About the Real Cost of Ownership
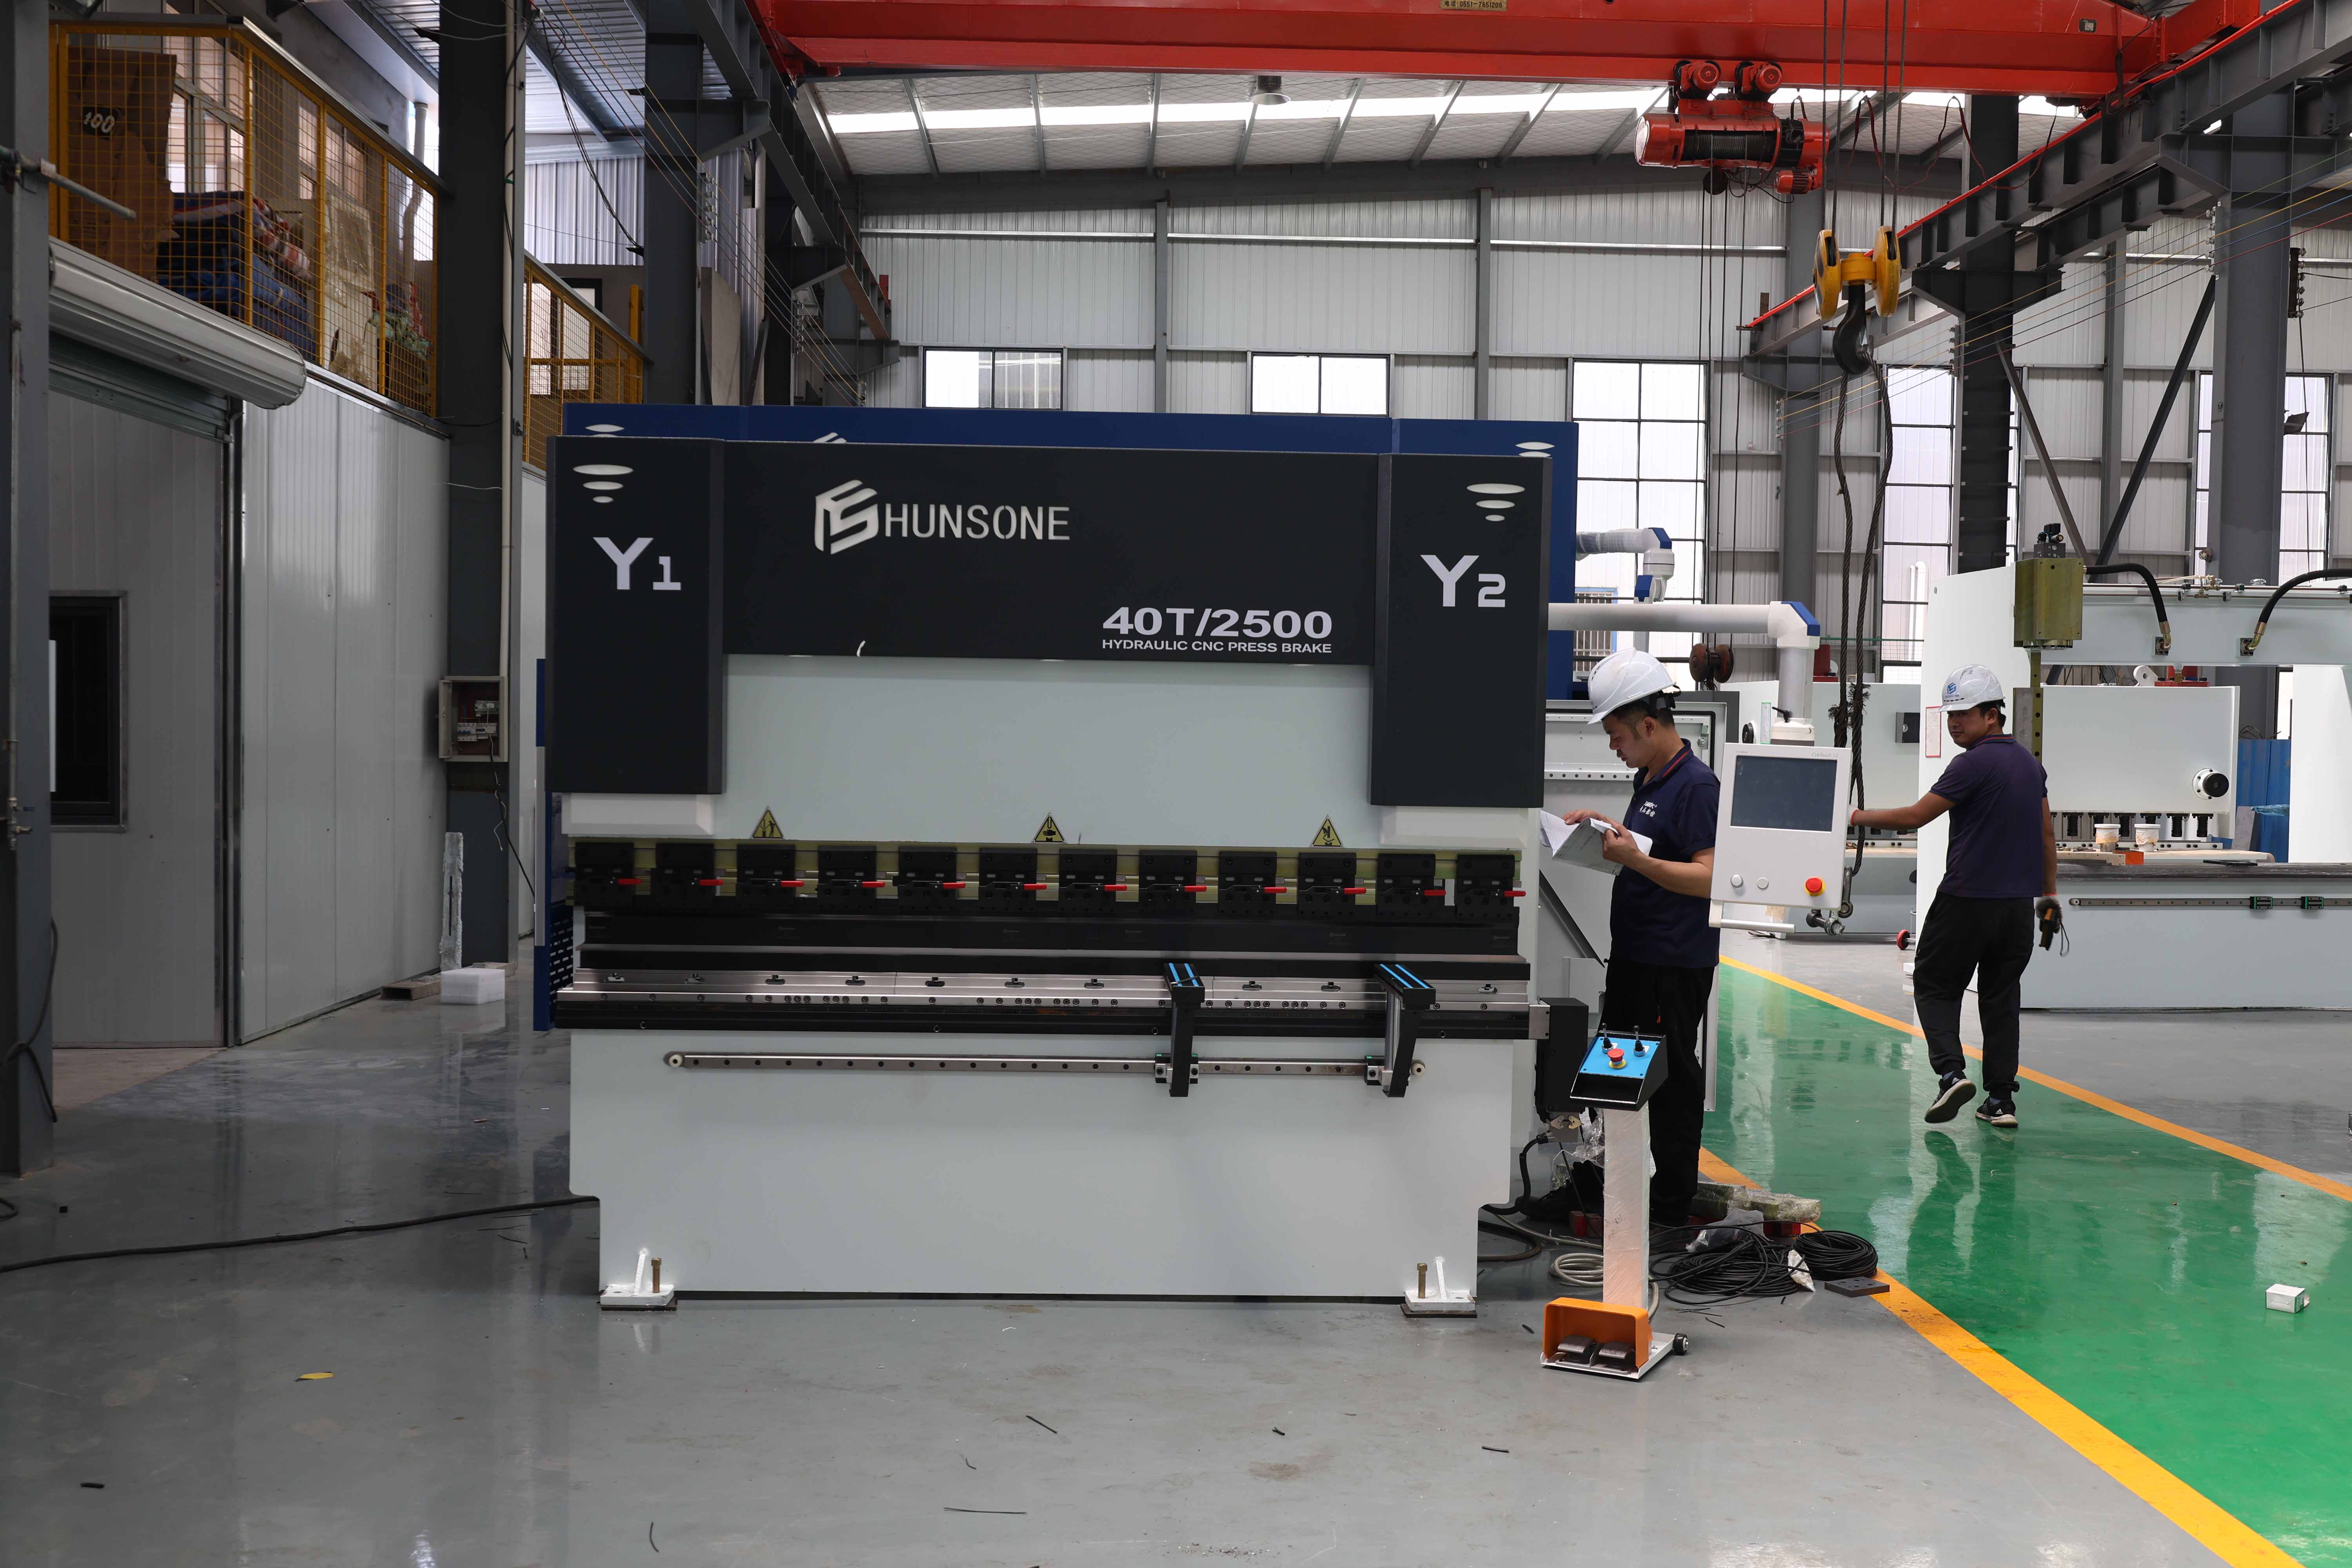
Ask anyone who has owned one for a couple of years and they'll tell you the sticker price is the easy part. The real cost shows up later, in small routine expenses that don't feel like much on their own but add up fast. Maintenance schedules, replacement filters, occasional software updates that require a service visit, and the higher insurance premium can quietly push the total well past what the brochure implied.
Some past buyers admit they underestimated how often they'd need to replace wear-and-tear items. A few mention that the first major service came earlier than expected, and the cost of genuine parts left them wishing they had budgeted an extra few hundred dollars a year. Others point to fuel or electricity consumption that was higher in real-world conditions than the official figures suggested, especially after the first year of ownership.
There's also the resale side. Several long-term owners note that depreciation hit harder than anticipated, partly because newer models arrived quickly and demand for older units dropped. If you plan to sell or trade in after three or four years, the gap between what you paid and what you get back can be the largest hidden cost of all. That's the number nobody puts on the showroom tag.
Which Tooling Configurations Match Your Specific Bending Needs
Pinpointing the right tooling setup starts with the bend radius your material can tolerate. Thin-gauge aluminum or stainless often demands a narrower V-die opening to achieve a tight, crisp radius without cracking, while heavier plate requires a wider opening to reduce tonnage and avoid over-stressing the press brake. The rule of thumb—using an opening roughly eight times the material thickness—works for many jobs, but high-tensile steels and alloys frequently push you toward a larger die to prevent edge fractures. Testing a short sample piece across two or three die widths reveals the exact configuration that holds the desired angle without marking the surface.
Beyond the V-die, punch selection shapes the outcome more than many realize. A standard straight punch handles most air-bending tasks, but acute-angle punches become necessary when springback is severe or when the final bend must exceed 90 degrees. For deep box bends or channels with return flanges, a gooseneck punch provides the clearance needed to avoid collisions. Pairing the punch nose radius to your material thickness—usually no smaller than the thickness for mild steel, and larger for harder alloys—prevents creasing along the bend line. The interplay between punch tip radius, die shoulder radius, and material hardness ultimately determines whether the bend comes out clean or shows witness marks.
Don’t overlook tooling height and clamping style when matching configurations to your machine. European-style quick-clamp systems let you swap segmented tooling in minutes, which is invaluable if your shop runs short batches with frequent changeovers. American-style tooling, while slower to set up, often provides greater rigidity for long, uninterrupted production runs. If your parts include multiple bends with varying flange lengths, a modular setup with different punch heights and die rail spacers gives the flexibility to handle everything from narrow channels to wide panels without re-tooling the entire bed. The best configuration is the one that balances precision, setup speed, and operator safety for the exact range of parts flowing through your shop.
Why Their Frame Design Tells You More Than a Spec Sheet
Look past the head tube angle and bottom bracket drop for a moment. The way a frame’s lines resolve—where a top tube tapers, how a seatstay curves into the dropout—gives you a sense of the builder’s priorities before you ever swing a leg over. A spec sheet can list tire clearance and wheelbase, but it can’t show you the slight bow in a fork leg that was added to take the sting out of chip-seal. It won’t tell you that the chainstays were shortened not just for snap, but because the designer wanted the rear wheel to tuck under a rider’s weight on a climb.
Tube diameters and joint transitions read like handwriting. A frame with a massive downtube and a paper-thin top tube isn’t just an exercise in stiffness numbers—it’s a statement about where the builder expects load to travel. Look closely at a lugged steel frame: the shape of the lug points, the filing marks left or polished away, even the choice of brass versus silver, hint at how the frame was intended to be ridden and maintained over decades. Those details never appear in a geometry chart, yet they shape every mile more than a stack-to-reach ratio.
Frame design is a record of compromises made visible. The dropout thickness, the cable routing choices, the placement of a pump peg or a third bottle mount—these aren’t random. They tell you whether the bike was built for a fast weekend century, a loaded tour across gravel, or a commuter that gets locked to a rack in the rain. A spec sheet gives you data points. The frame gives you the story behind them.
Where They Source Hydraulic Components and Why It Changes Everything
The map of hydraulic component sourcing rarely follows a straight line. Many operations lean on regional distributors for urgent replacements and overseas manufacturers for volume orders, but the real shift has been quieter. Suppliers in northern Italy, Slovenia, and a handful of Japanese industrial towns now account for a surprising share of custom-machined blocks and cartridge valves. These aren't the cheapest on a spreadsheet, yet they win repeat orders because their dimensional consistency holds up after months of thermal cycling.
A stubborn pump or a valve that fails under pressure seldom gets blamed on where it was bought, though that is often where the trouble begins. Shops that pull from multiple tiers, some direct and some through brokers, end up with tolerances that do not match, coatings that wear unevenly, and seals that look right but harden early. The invoice might look lean, but the hidden cost appears later, when a crane sits idle and the only replacement that actually fits is still three time zones away.
That is why sourcing has moved from a purchasing chore to an engineering decision. Teams that trace component origins and stick to suppliers who document casting and heat treatment tend to run longer between teardowns. Warranty claims drop, rebuild cycles stretch, and the maintenance budget stops swinging wildly from quarter to quarter. Where the parts come from changes more than the bill. It changes how often the equipment has to stop.
When You Can Actually Expect Delivery Without the Runaround
Most retailers quote delivery windows that stretch like taffy, but the honest answer lies in how their logistics actually function. When a company owns its fulfillment centers and uses regional carriers instead of drop-shipping from a third party, you stop seeing the dreaded “5 to 10 business days” that always turns into two weeks. Look for language that mentions dispatch cutoff times, real-time tracking that updates at every scan point, and delivery estimates tied to your ZIP code rather than a vague national average. If the checkout page asks for your location first and then gives you a date range of two or three days, you’re likely dealing with a system that isn’t guessing.
The runaround usually happens when multiple middlemen are involved. A seller who ships from a warehouse they’ve never seen, using a carrier that hands your package to a local courier, is setting you up for “attempted delivery” notices and mysterious delays. On the other hand, brands that promise delivery without runaround typically show a map of their warehouse locations, offer a single tracking number that never changes hands, and provide a phone number that a real human answers when something goes sideways. Check if the delivery date is backed by a guarantee—not the kind that forces you to fill out a form and wait thirty days, but one that automatically refunds shipping or sends a replacement if the package is late.
Another telltale sign is how the company handles exceptions. If your order is stuck in a snowstorm or a customs hold, do they proactively email you with a new date, or do you have to chase them through chat bots and email threads? Delivery without the runaround means the seller treats your time as part of the product. They use route optimization to avoid failed first attempts, allow you to pick a delivery window on the day of arrival, and never ask you to “contact the carrier directly.” When you see all of that working together, you can actually believe the date on the confirmation screen.
FAQ
Ask for the calculation. The rep should review your thickest material, widest flange, and die opening. If they jump straight to the largest model, that's a red flag.
Don't settle for a vague 'many.' Get real numbers and a couple of local references. Talking to an operator beats reading a brochure every time.
Look for hands-on training at your facility, not just a manual. A realistic answer is two to five days for basic programming and setup, with follow-up calls included.
Push for specifics: same-day phone support, 24-hour technician dispatch, and a parts warehouse in your region. If they hesitate, expect downtime later.
A good company will suggest a quick-change clamping system and segmented punches rather than selling you every accessory. Ask them to justify each line item.
Get a line-item breakdown. Some vendors hide rigging and electrical hookup charges until the machine shows up. Confirm who handles the forklift and final leveling.
If they have a demo room, send them your drawing and material. Watching the actual bend angle, cycle time, and operator interface tells you more than any spec sheet.
Conclusion
Before you commit to a press brake manufacturer, dig into how they handle downtime. A company that hesitates to describe its service response—who answers the phone at 2 a.m., where spare parts are stocked, and whether technicians travel from the same region—will cost you far more than the machine itself. Ask past buyers about the full cost of ownership, not just the invoice. Blade wear, hydraulic oil changes, unexpected electrical faults: these line items surface only after months of production. Tooling compatibility matters too. A supplier should match clamping systems, punch heights, and die shoulders to your bending radii, not push a one-size-fits-all package.
Equally revealing is how the frame itself is built. Thicker side plates, welded stress relief, and crown compensation tell you whether the machine holds angle accuracy after years of off-center loads. Ask where hydraulic components come from. Valves and pumps from a known OEM often mean easier rebuilds and less downtime than no-name parts. Finally, pin down delivery. A real manufacturer can give you a production slot, a serial number, and a firm date—not weeks of vague updates. When these details line up, you’re no longer shopping for a spec sheet; you’re choosing a production partner.
Contact Us
Contact Person: James Chen
Email: [email protected]
Tel/WhatsApp: 86 13770803946
Website: https://www.hunsone.com/