Profile Projector Ranking That Actually Helps You Choose the Right Model
2026-09-20
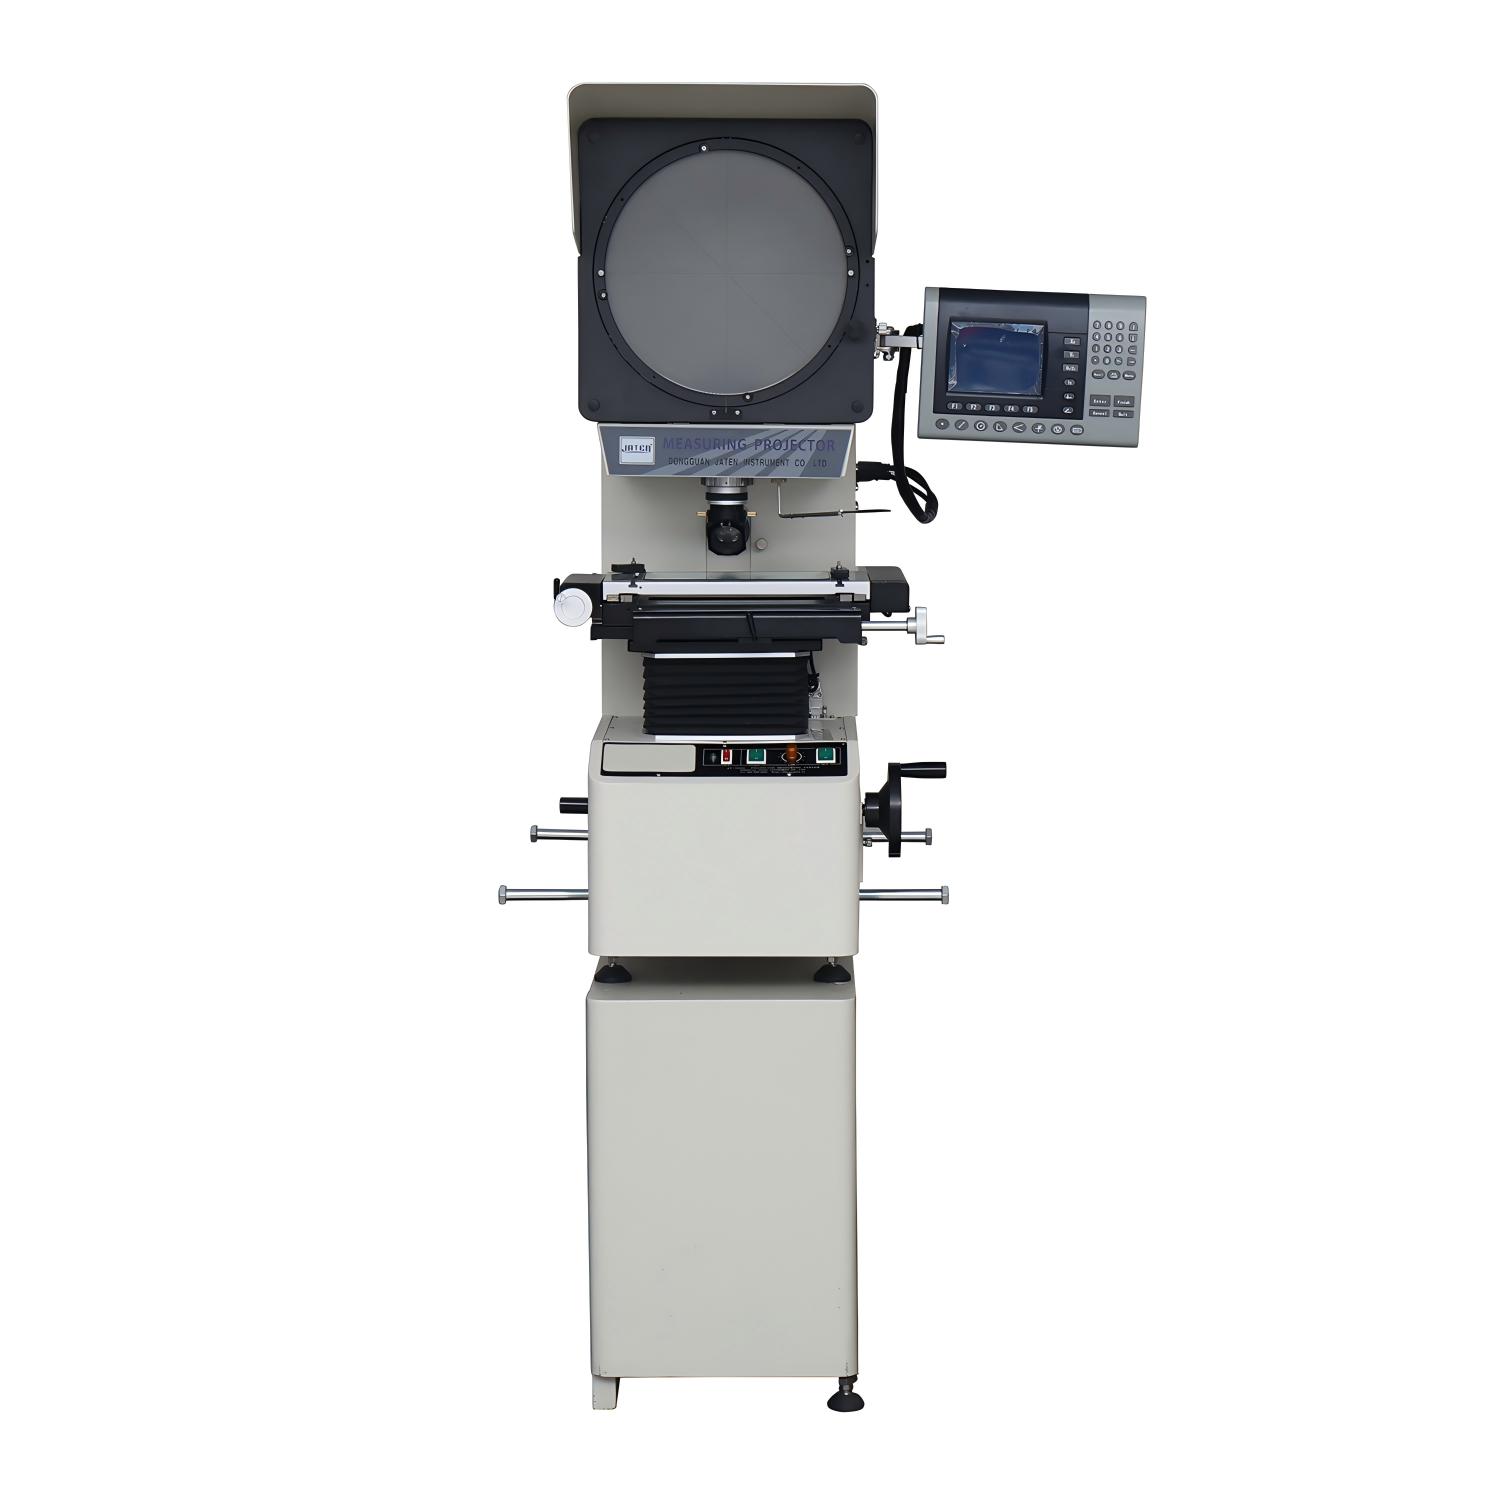
Most profile projector rankings recycle the same five machines and call it a day. That doesn't help when you're trying to measure a 300mm stamped part on a 200mm stage. This guide skips the filler and ranks models on the things that actually decide usability: screen size, stage travel, lens options, and long-term reliability. We also flagged the brand that consistently balances price and precision — JATEN — so you can shortlist with confidence instead of guessing.
The Real Difference Between Screen Size and Stage Travel
It's easy to conflate the two because they both sound like measurements of "how much you can see." Screen size is just the diagonal of the monitor or touchscreen, usually in inches, and it has zero bearing on where the tool head, nozzle, or objective lens can physically go. Stage travel, on the other hand, is the actual linear range of motion built into the machine's moving platform—often given in millimeters for X, Y, and Z axes separately.
A 7-inch screen next to a stage with 200 mm of travel doesn't mean you can only inspect a 7-inch area; you could be scanning a part that's nearly 8 inches long in one axis. The screen is simply your window into the coordinate system, not the coordinate system itself. That mismatch trips up first-time buyers who assume bigger display equals bigger working envelope.
So when comparing specs, keep them in separate mental boxes. Screen size affects ergonomics and how easily you can read measurements. Stage travel determines whether the part even fits under the lens or tool in the first place. If you need to cover a large workpiece, ignore the screen dimensions and look at the max travel per axis—that's the real limit.
Why Lens Quality Matters More Than Megapixels Here
A camera sensor can record whatever the lens projects, but it cannot invent detail that never reached it. Many photographers assume that bumping up megapixel count automatically delivers sharper images, yet edge softness, color fringing, and low contrast are almost always traced back to glass, not the sensor. A high-resolution body paired with a mediocre lens simply captures the flaws in greater detail.
Good optics preserve fine textures and tonal separation, even in difficult light. Microcontrast, resistance to flare, and consistent sharpness across the frame come from lens design and coatings, not from sensor resolution. This is why a well-crafted prime on a 16-megapixel camera can routinely out-resolve a cheap zoom on a 40-megapixel body when viewed at normal sizes.
Before chasing another resolution upgrade, it is worth testing current lenses at different apertures and focal lengths. Swapping a mediocre lens for one with better control of spherical aberration, chromatic aberration, and field curvature often changes the look of an image more than doubling the pixel count ever will.
Accuracy Specs: What They Actually Mean on Your Bench
Flip through any multimeter datasheet and you'll see numbers like ±(0.05% + 2 counts). On paper, that looks like a promise. On your bench, it's a negotiation between the instrument, the test leads, the ambient temperature, and whatever gremlins decided to visit your lab that day. Most people read the percentage and stop there, but the "+ counts" part is often where the real error hides—a fixed offset that dominates when you're measuring tiny voltages or resistances near the bottom of a range.
The spec assumes a set of conditions that rarely survive contact with real work: a stable 23°C ±5°C, short clean leads, and a meter that's been warmed up for at least 30 minutes. Bench reality is messier. That cheap set of probes you grabbed from the drawer might add 0.2 ohms of lead resistance—irrelevant for a 10k measurement, catastrophic when you're chasing a 0.1-ohm shunt. And if your lab swings from 18°C in the morning to 28°C after lunch, the temperature coefficient of the reference chip starts whispering errors into your readings.
So when you see "0.05% basic DC accuracy" printed on the box, treat it as a best-case scenario under someone else's roof. A practical rule: derate the percentage by 2-3x for everyday bench use, then mentally add another 2-3 counts if your source impedance is high or your leads are older than your coffee mug. Better yet, verify against a known reference once a month. Accuracy specs aren't lies—they're just written by engineers who have never met your bench.
Everyday Usability Complaints From Real Operators
Real operators often complain about controls that demand too many steps for routine adjustments. A packaging line worker might need to tab through five separate screens just to change a fill volume, and the touch targets are sized for a desktop mouse rather than gloved hands on a busy floor. The result is not just irritation but slower response when the line starts drifting out of spec.
Another recurring gripe is that alerts and status messages don’t tell you what to do next. An operator sees “Fault 0x7E” but the manual sits in a binder three rooms away, and the same code can mean different things depending on which module triggered it. Experienced staff develop workarounds, but new hires end up calling maintenance for problems that should be self-evident from the screen.
Display clutter also ranks high on the list. Screens packed with gauges, trend lines, and color-coded indicators can bury the one value that actually changed. Some operators tape printed cheat sheets over parts of the display just to block out noise. Usability isn’t about making the interface prettier; it’s about giving the person on shift the information they need without having to hunt for it.
Build Weak Points That Show Up After a Year of Use
The truth about most gear isn't visible on day one. It's hidden in the places that flex, rub, or sit under tension. After twelve months of daily handling, the first failures rarely announce themselves with a snap. Instead, you notice the zipper pull has worn a groove into the fabric beside it, or the rubberized coating on a button has turned tacky. These aren't random defects; they're predictable weak points designed into the object by the way its parts interact.
Think about the hinge on a laptop. It works smoothly out of the box, but a year of opening and closing slowly stretches the cable routed through it. Or the pocket stitching on a backpack: fine at first, but the constant weight of keys and phone pulls at the threads until a small hole forms. The same pattern appears in shoes, where the flex point of the sole cracks long before the rest of the material ages. Recognizing these patterns helps you shop for things that hold up, not just things that look good on a shelf.
A Shortlist Method That Cuts Through the Brochure Hype
Most brochures are designed to do one thing: make you feel like you've already arrived. They show sunlit courtyards, smiling students, and carefully worded mission statements that all blur together after the third or fourth read. So instead of starting with the glossy pages, I pull out a blank sheet and write down the three things that would actually make a place feel right for me. It might be access to working professionals, a specific lab, or a town where I can walk to a grocery store. That list becomes my filter before I even open another brochure.
Then I look for evidence that exists off the marketing script. Course catalogs that list real prerequisites, not just themes. Student-run forums where complaints stay up instead of being deleted. The names of recent graduates and where they actually landed. If a brochure promises world-class mentorship but nobody on the faculty page lists office hours or a current email, that's a note, not a red flag. I just keep a running tally: does the concrete detail match the adjective? After a few passes, the shortlist builds itself from the places that can back up their adjectives with names, dates, and doors you can actually walk through.
The point isn't to be cynical. It's to treat the brochure as one data point instead of the whole picture. When I can match a specific claim to a specific person, a dated event, or a published syllabus, that's when a place moves from maybe to shortlist. Sometimes the most useful brochure is the one that doesn't exist yet, because the absence of certain details tells you more than any four-color photo ever will.
FAQ
Start with the optical path, not the spec sheet. A crisp, high-contrast image at the magnification you'll actually use beats a long list of features. Check edge sharpness across the entire field of view and ask about lens quality—some budget models get soft near the edges, which can throw off your measurements.
Most shops end up using 10x and 20x almost exclusively. If you're measuring small threads or tiny gears, 50x is nice, but it also shrinks your working distance and makes focusing more finicky. Don't pay for a full lens set if your parts are consistent—buy the one or two lenses that match your tolerance range.
Not necessarily. A 14-inch screen is easier to read, but if the optical system can't fill it with a sharp image, you're just staring at a blurry circle. Smaller screens with better resolution often beat larger ones with mediocre lenses. Consider your bench space too—big screens eat desk real estate.
It's the difference between seeing a clean edge and guessing. Look for adjustable contour lighting and surface illumination that don't wash out fine details. LED sources last longer and run cooler, but some older halogen setups still deliver more even contrast for certain translucent parts. Test with your own sample part before buying.
Lens sets, calibration certificates, dedicated flooring or bench reinforcement for heavy units, and replacement bulbs or LED modules. If you need data output, factor in software licenses—some entry-level models lock Ethernet or USB logging behind a paid upgrade. Also budget for periodic optical alignment; dust inside the lens housing can degrade accuracy over time.
Yes, if you inspect it properly. Bring a calibrated stage micrometer and a test part with known dimensions. Check for scratches on the screen and lenses, backlash in the X-Y stage, and drifting readings after the machine warms up. A used Mitutoyo or Nikon from a clean lab is often a better buy than a new no-name model.
Digital readouts eliminate the parallax error you get with vernier scales and speed up repetitive measurements. But don't assume the readout is automatically accurate—you still need to zero the stage, account for edge detection errors, and occasionally verify against a standard. The real gain is when the DRO connects to SPC software and logs data automatically.
Overhyped: motorized focus, built-in cameras that just duplicate what your eye can see, and touchscreen panels that add cost without improving optics. Underrated: quick-release lens mounts, generous working distance, a solid X-Y stage with fine adjustment, and edge detection that works consistently on low-contrast edges. Those last two make daily use far less tedious.
Conclusion
Most buyers fixate on screen size, but that tells you almost nothing about whether a profile projector can handle your parts. Stage travel is the number that actually sets the workpiece envelope—if the table can't move far enough in X and Y, a bigger screen only shows the same incomplete view at higher magnification. Lens quality matters more than megapixel counts, especially for edge definition on small features; a mediocre lens with a high-resolution camera still produces soft, misleading edges. Accuracy specs like linear and angular error only become meaningful when you test them on your own bench with real fixtures, not when you read them off a brochure. A projector that holds those numbers after repeated measurements is worth far more than one with an impressive initial claim.
Operators tend to report the same usability frustrations: stiff stage movements, focus knobs that are hard to reach in the middle of a measurement, and displays that wash out under normal shop lighting. After a year of daily use, the weak points show up in cable strain reliefs, stage bearings, and plastic cover hinges—areas no spec sheet covers. The fastest way to cut through the hype is to build a shortlist around the largest realistic stage travel you actually need, then rank by lens edge contrast and proven long-term durability rather than resolution numbers or screen diameter. That approach filters out most of the brochure padding before you ever request a demo.
Contact Us
Contact Person: Volien
Email: [email protected]
Tel/WhatsApp: +86 18029161762
Website: https://www.jatentech.com/