Thermal Printable Wristband Factory Guide for High-Quality Custom Orders
2026-09-25
Ordering custom thermal printable wristbands looks straightforward—until a shipment arrives with smeared text, weak adhesive, or barcodes that won't scan. If you've ever had to trash thousands of unusable bands, you already know the real problem isn't the design; it's the factory behind it. This guide cuts through supplier noise and focuses on the production details that separate dependable custom orders from costly mistakes, using BAOBI as a reference point for quality you can actually verify.
How Thermal Wristbands Handle Water, Sweat, and Long Wear
Thermal wristbands are built with a sealed, multi-layer construction that keeps moisture from reaching the heat-sensitive core. A flexible polyurethane outer shell repels splashes and light rain, while a hydrophobic inner lining wicks sweat away from the skin. This double barrier means a quick handwash or a sweaty workout won't short out the heating element or cause uncomfortable dampness against your wrist.
Even with constant movement and daily wear, the materials resist cracking and delamination. The silicone-based adhesive used between layers stays flexible through temperature swings, and the edge bonding is reinforced to prevent peeling. So whether you're typing for eight hours, running errands in damp weather, or sleeping with the band on, the thermal function remains stable without any sticky or soggy spots.
Long-term exposure to sweat and skin oils is handled by the anti-microbial inner fabric, which stops odor buildup and irritation. The wristband doesn't need special drying routines—wiping it down with a dry cloth after heavy sweating is enough. Over months of use, the heating performance stays consistent because the sealed electronics never come into direct contact with moisture, and the outer coating resists yellowing or stiffening from repeated exposure to water.
Custom Printing Methods That Keep Barcodes and Text Sharp
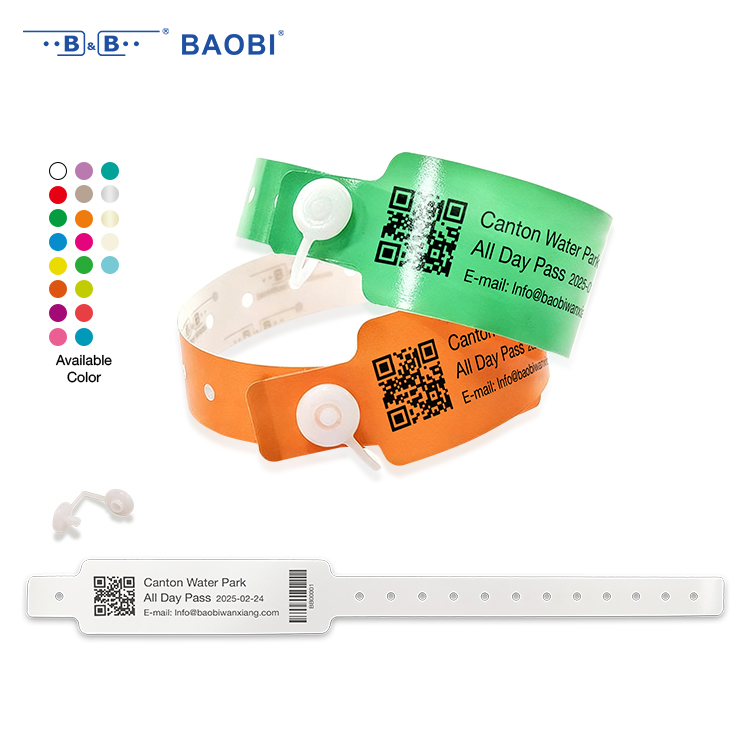
When barcodes start to blur, scan failures follow quickly. Unlike standard printing, where a slight loss of edge definition is tolerable, custom methods put the burden back on the substrate and ink combination. Thermal transfer on coated paper, for instance, forces the ribbon to release cleanly into the surface, preventing the wicking that turns crisp bars into fuzzy streaks. Adjusting heat and speed together matters more than either setting alone — too fast and the ink sits on top, too slow and it bleeds sideways.
Laser engraving changes the equation entirely. Because it burns away a top layer rather than depositing pigment, the resulting code is physically recessed, so it stays sharp even after exposure to solvents, abrasion, or repeated handling. The trick is matching the focal depth to the material: metals tolerate a tighter beam than plastics, and getting that wrong causes charred edges that scanners misread as extra bars.
For inkjet on porous stock, sharpness depends on controlling droplet spread before it dries. A quick pre-coat or a thicker ink with slower penetration can keep the dot pattern from merging into a solid mess. Testing under your actual scanning conditions — same angle, same lighting, same reader — remains the only honest way to confirm that the method you chose keeps both text and barcode legible after weeks in the field, not just on the first sample off the line.
Choosing the Right Adhesive and Coating for Your Environment
Temperature swings, humidity levels, UV exposure, and chemical contact all shape how well an adhesive or coating performs over time. In outdoor settings, for instance, picking a formula that withstands thermal cycling and UV degradation often matters more than chasing the highest initial bond strength. Start by checking the service temperature range and chemical resistance data in the product datasheet, and treat vendor marketing claims as secondary to your own field testing.
Substrate type plays an equally important role. Porous surfaces like concrete or wood need different wetting behavior than metals or plastics, which may require a primer to promote adhesion. Running small test coupons under real working conditions tells you far more than generic manufacturer advice. Many bond failures trace back to overlooked surface energy differences or skipped cleaning steps, so don't underestimate preparation.
Application method and curing constraints deserve early attention too. Some adhesives demand precise mix ratios or extended cure times, while coatings may need controlled thickness to hit their protection targets. Instead of reaching for a so-called universal product, clarify your production rhythm and on-site handling limits first. Then ask suppliers to recommend a few candidates matched to those constraints, and run side-by-side trials before committing to a full-scale rollout.
The Artwork Details That Delay Your Wristband Order
Most delay issues start innocently enough—something like a logo file that looks sharp on a phone screen but falls apart the moment it's scaled to wristband size. Tiny text, thin outlines, and layered effects that seem fine in a digital mockup often become unreadable or muddy when printed on the flexible, narrow surface of a wristband. If you want to keep production moving, stick to bold, simple vector art with solid colors and clear contrast.
Another common slowdown comes from color matching. Pantone references, metallic foils, or exact brand shades can trigger rounds of back-and-forth proofs, especially when a file uses RGB colors instead of CMYK. Gradients and shadows also tend to print inconsistently on woven or silicone bands, so designers sometimes have to flatten or simplify those details before the order can proceed.
Finally, custom effects like embossing, debossing, or full-color edge-to-edge printing add steps to the approval process. If the artwork includes critical details near the edges, they may need to be pulled inward to avoid being cut off during die-cutting. The quicker you resolve these layout quirks, the sooner your wristbands leave the production queue.
Wristband Defects You Won't Notice Until It's Too Late
Most people check a wristband for obvious tears or broken clasps before wearing it. The real trouble starts in the spots you never look: the inner edge of the adjustment holes, the thin strip behind the buckle, or the adhesive seam where the fabric meets the plastic. These areas flex constantly against your skin and sweat, and by the time a visible crack shows up, the band has already been weakening for weeks. You'll feel it first as a slight looseness, then suddenly one afternoon the band just lets go mid-activity.
Another late-blooming defect hides in the coating. Silicone and synthetic leather bands often start with a smooth, matte finish that slowly picks up a tacky, almost sticky feel. It doesn't look wrong at first; you might blame hand lotion or humidity. But that tackiness is the outer layer breaking down, and once it starts, it attracts lint and skin oils faster than you can clean it. The band will begin to smell faintly sour no matter how often you wash it, and the color will dull unevenly where it touches your desk or wristbone.
Then there's the hardware you trust without thinking. A stainless steel loop can develop microscopic burrs along its inner edge after months of friction against the band's tail. Those burrs gradually shave away the band material, leaving a pale, thin line you won't notice until the strap tears through at the very point where you tuck it in. Magnetic clasps are worse: the plating wears off in patches, exposing a dull core that doesn't hold as tightly, so the band starts slipping open when you bend your wrist back. None of these failures announce themselves with a loud snap; they creep in quietly and catch you only after the damage is already done.
Small-Batch vs Bulk Pricing and Lead Time Differences
When comparing small-batch orders to bulk purchases, the pricing gap often extends beyond a simple per-unit discount. Bulk pricing typically reflects lower setup costs spread across more units, but small-batch buyers may also face hidden surcharges for line changes, dedicated tooling, or expedited material sourcing. In many supplier catalogs, the quoted price for a single prototype can be three to five times higher than the per-unit cost at 1,000 pieces, yet this multiplier isn't always linear. For example, a 100-piece order might sit only 20% above the bulk rate if the supplier already runs similar jobs, while a 10-piece order could carry custom setup fees that erase any volume discount entirely.
Lead time differences follow a similar nonlinear pattern. Bulk orders often slot into optimized production schedules with weeks of buffer, whereas small-batch runs may be squeezed between larger jobs or held until a minimum batch is reached. A surprisingly common scenario: a 50-piece order waits two weeks longer than a 5,000-piece order because the factory batches small orders from multiple clients into a single setup. Conversely, some suppliers reserve rapid-response capacity for prototype-scale quantities, meaning a 20-piece order could ship in five days while a 500-piece order takes three weeks due to material procurement and line scheduling.
To navigate these differences, buyers should request tiered quotes across multiple quantity breakpoints rather than assuming a smooth price curve. Ask explicitly about setup amortization schedules and whether small batches are consolidated with other customers' orders. For lead times, inquire about the supplier's batching policy—do they run small orders weekly, biweekly, or only when a critical mass accumulates? The answers often reveal that the most cost-effective order size isn't the largest, nor the smallest, but the one that aligns with the supplier's existing production rhythm.
FAQ
Check whether they produce materials in-house or act as a trader. A real factory usually runs extrusion or coating lines and can supply material data sheets. Ask for a sample book and confirm they support barcode/QR test prints. Don't judge by price alone; verify slitting tolerance and printhead wear testing before shipment.
Synthetic paper feels closer to regular paper and works for short events at a lower cost. Polypropylene resists tearing and water better, so it suits pools, water parks, or multi-day festivals. If guests will touch sweat or sunscreen, go with polypropylene; for simple check-in entry, synthetic paper is enough.
Color count, print coverage, and size changes make the biggest difference. Spot colors usually cost less than full process color, but going beyond three spot colors raises the price. Adding punch holes, tear lines, or sequential numbering also increases tooling or process costs. The most economical route is using an existing die size and one or two spot colors.
Good polypropylene wristbands can handle continuous soaking, chlorine, and sunscreen, but the adhesive matters. Ask the factory for strong hot-melt adhesive or ultrasonic welded closures instead of standard double-sided tape. The thermal layer itself is not waterproof, so the surface needs a protective film, otherwise moisture will fade the print.
The most common problems are fuzzy barcode edges and white spots in solid black areas. This usually comes from uneven thermal coating or wrong printer temperature settings. After getting samples, test with your actual printer and check 100% black blocks and the smallest barcode density. Ask the factory if they have coating sensitivity recommendations for low-energy or high-energy printers.
Proof approval usually takes 2-4 days, production runs 7-12 business days, and shipping is separate. If you need special inks or custom tooling, add another 3-5 days. During peak season, like before summer festivals, allow double the lead time because factory schedules can fill up fast.
Most factories set a minimum between 5,000 and 10,000 pieces, but some accept 1,000-piece orders at a much higher unit price. If you only need a few hundred, consider buying blank wristbands and thermal printing them yourself instead of pre-printing.
Common mistakes include using low-resolution images, forgetting to convert text to outlines, and not leaving a safe area for punch holes or tear lines. Submit files in vector format like AI or PDF, keep text at least 3 mm from the edge, and align barcodes with the printhead feed direction, otherwise scanning will fail.
Conclusion
Thermal printable wristbands for events, hospitals, and venues need to survive more than a quick scan. The factory process starts with a top-coated thermal layer that resists water and sweat, so text and barcodes don't smear after a shower or a humid shift. Sharp output comes from pairing a high-resolution thermal printhead with a smooth, non-porous surface, which keeps even dense 1D barcodes readable after repeated flexing. The adhesive and coating are chosen together, so a soft acrylic adhesive works for sensitive skin and short wear, while a stronger rubber-based adhesive with a matte or glossy overlaminate suits pools, gyms, or outdoor events. If you need wristbands to last multiple days, ask for a thicker film or a reinforced tamper-evident closure rather than relying on standard paper stock.
Artwork delays usually come from small file issues, not complex designs. Missing bleed, tiny font sizes, or low-resolution logos are the main reasons a proof bounces back, adding days to production. Many buyers only notice defects after the bands are printed and shipped, such as uneven coating, adhesive that leaves residue on skin, or a barcode that fades in direct sunlight. These problems are invisible on a digital proof. Before committing to a large run, order a physical sample and bend it, wet it, and scan it under the same lighting the venue will use. Pricing changes sharply between small batches and bulk orders. Under 5,000 pieces, the setup and plate fees dominate, so the unit price looks high. Above 10,000 pieces, the cost per band drops but lead time stretches because of die-cutting and coating changes. A factory guide that doesn't explain this split leaves customers comparing quotes that aren't actually comparable.
Contact Us
Contact Person: Bill Xu
Email: [email protected]
Tel/WhatsApp: 8618688898707
Website: https://www.baobitech.com/