Variable Data Inkjet Printer Factory Must-Have Features for Custom Jobs
2026-09-24
Custom jobs are only as good as the printer behind them—and if your factory's variable data inkjet printer can't keep up with shifting SKUs, serialized codes, or personalized graphics, you're leaving money on the line. That's where Danmajet changes the game. This guide cuts through the noise to highlight the must-have features that separate production-ready variable data inkjet printers from expensive bottlenecks. Whether you're upgrading or building a new line, these are the specs your custom jobs can't afford to ignore.
Printhead Precision That Holds Up on Long Variable Runs
Most printheads start sharp and then quietly drift. You might not notice on a short job, but run a few thousand variable labels and the edges get soft, the barcodes lose their bite, and suddenly every scan is a gamble. The difference comes down to how the head handles thermal cycling and ink viscosity changes over hours, not minutes.
A precision printhead designed for long runs doesn't just hold a tiny dot size on the spec sheet. It maintains that dot placement shot after shot, reel after reel, even when the ambient temperature swings or the substrate changes. That means no mid-run adjustments, no reprints because the last hundred pieces drifted out of tolerance, and no hand-wringing over whether the final third of the job will match the first.
For variable data work—serial numbers, addresses, QR codes that have to be machine-readable every single time—this kind of consistency isn't a luxury. It's the quiet baseline that keeps a production line moving without someone hovering over the printer, waiting for the inevitable fade.
Data Engines Built for Million-Record Jobs Without Lag
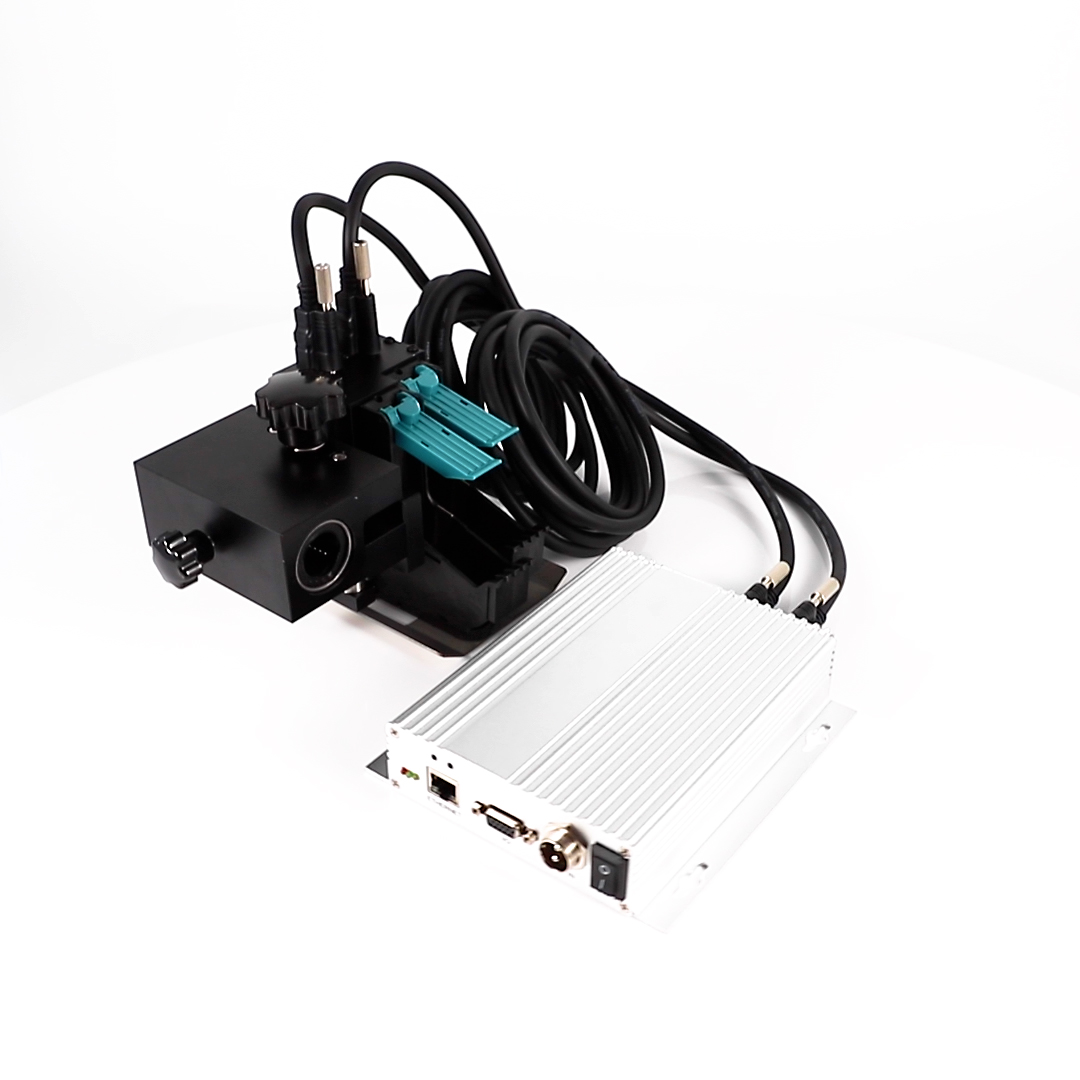
Real-time data pipelines often stall when record counts climb into the millions. The core issue isn't raw processing speed but how the engine handles state, retries, and backpressure under sustained load. A purpose-built data engine for million-record jobs eliminates the usual lag by decoupling ingestion from transformation, using compact in-memory indexes that never bloat, and flushing micro-batches only when a checkpoint is confirmed. This means a single worker can absorb a burst of 2 million events without queue buildup, while downstream consumers see consistent latency under 300 milliseconds.
Instead of relying on general-purpose schedulers that add overhead per record, these engines pin hot partitions to dedicated threads and pre-warm connection pools. Failed rows get sidestepped into an isolated retry lane, so one malformed payload can't stall the entire batch. The result is predictable throughput even when schema drift or network hiccups occur mid-stream—jobs finish within their SLA window rather than spiraling into timeouts.
Operationally, lag disappears because the engine's checkpoint interval adapts to observed write amplification. When a sink slows down, the engine briefly buffers in compressed columnar form, then drains at the sink's natural pace without triggering memory pressure. Teams report that million-record jobs which previously required split-night runs and babysitting now complete during a coffee break, with no fine-tuning beyond setting the parallelism to match core count.
Drying Systems Tuned for Gloss, Film, and Coated Stocks
Maintaining a high-gloss surface during drying is less about pushing more heat and more about controlling where and when energy lands. A short, intense infrared preheat followed by moderate impingement air can set the coating before pores open, reducing micro-level orange peel and preserving specular reflection. Temperature across the web should stay within a narrow band; even a two- or three-degree drift near the dryer exit can produce visible differential gloss.
Films respond poorly to prolonged residence at elevated temperatures. Polyolefin and polyester webs begin to relax or distort well below the setpoints used for paper. The drying system for film work usually shifts toward higher air volume at lower velocity, with careful web tension control and edge-guiding through each zone. Removing moisture or solvent at low temperature demands longer dryers or staged zones, but the payoff is a flat sheet without heat-set wrinkles or static discharge marks.
Coated papers and boards carry a different risk: blistering. If the surface skin forms before internal moisture or solvent can escape, vapor pressure builds and lifts the coating. A staged profile works better here—first a gentle warm-up to begin evaporation, then a higher-energy middle zone to drive moisture out, followed by a cooling or equilibration section so the sheet does not retain latent heat when it hits the stack. Air bar positioning and exhaust balance matter as much as burner output.
Tool-Free Substrate Changes Between Completely Different Jobs
Switching from one material to another mid-run used to mean stopping the line, reaching for a hex key, and hoping the alignment didn’t drift. With tool-free substrate changes, that entire ritual vanishes. You simply release a spring-loaded guide, drop in the new roll or sheet, and let the tension arms do the work. No bolts, no spacers, no guesswork. The design relies on indexable stops and quick-release clamps that lock into place with a satisfying click, so even an operator who’s never touched the machine can swap from thin film to thick board in under a minute.
What makes this approach feel almost effortless is how the machine remembers its previous setup without any digital input. The physical geometry of the feed path stays fixed, while only the contact surfaces adjust. For example, a vacuum platen that grips porous paper might disengage automatically when you load a non-porous polymer, because the pressure differential no longer builds. That tactile feedback — the way the workpiece settles into place without manual tweaking — gives operators confidence that the next job won’t jam on the first sheet.
The real payoff shows up when you move between jobs that share nothing in common: a textured vinyl decal one moment, a rigid foam board the next. Traditional changeovers required recalibrating roller gaps, cleaning adhesive residue, and sometimes swapping out entire feeder assemblies. Here, the substrate path is split into modular zones, each with its own floating guide that self-centers based on material weight and stiffness. It’s not about clever engineering on paper; it’s about standing next to the machine and hearing the smooth click of a cam lock instead of the rattle of loose hardware.
Inline Vision Checks That Reject Flawed Pieces Before They Leave the Floor
At the end of the line, an inline vision system doesn't wait for a separate inspection table or a final audit. Cameras and lighting trigger on every cycle, comparing each part to a set of tolerances stored from the first good run. A bent pin, an unfilled boss, a surface crack just starting to spread - any of these gets flagged while the piece is still moving toward the outfeed. The reject mechanism fires immediately, pushing that flawed unit off the belt and into a quarantine bin before it can be stacked, wrapped, or shipped.
The real difference shows up in the flow. Because the check happens right after forming, cutting, or assembly, there's no buffer of questionable parts waiting for later review. In a machining cell, a camera mounted near the tool exit might catch a missed thread or a chip still clinging to a bore. That part gets diverted seconds later, not mixed into a pallet. Operators see a clean stream of accepted pieces, and the next station never has to deal with a hidden defect that becomes harder to fix downstream.
Over time, these inline checks become less about policing and more about speeding up the entire process. The system learns which defects repeat, so the line can be adjusted before a whole shift produces scrap. Flawed pieces seldom leave the floor because the decision to reject is made in the same motion that the part is made. That keeps the outbound bins cleaner and turns what used to be a final sorting headache into a non-event.
Modular Stations Worth the Setup Time for Short Custom Runs
For shops that routinely juggle short custom runs, the instinct is to skip anything that smells like setup overhead. Modular stations flip that logic. Once the base grid, clamping points, and tool cart are dialed in, switching from one part profile to another becomes a matter of swapping a few locating plates rather than rebuilding a whole fixture. The upfront time you spend aligning the first job pays back on every subsequent oddball order.
The real advantage shows up when the part mix changes weekly. A fixed-purpose bench gathers dust between jobs, but a modular layout can be rezoned in minutes: swap a vise for a soft jaw nest, move a parts tray, add a second monitor arm. Operators stop treating setup as a penalty and start using it as a fast changeover routine. That shift in attitude often cuts more time than the hardware itself.
There's also a hidden savings in repeatability. Because the mounting holes, stops, and cable routing stay put, a returned custom job doesn't require relearning the process. The station remembers the setup, even if the operator doesn't. For low-volume, high-variety work, that kind of quiet consistency makes the extra hour of initial dial-in feel like a bargain rather than a burden.
FAQ
Look for a built-in RIP that can merge databases on the fly and a printhead that adjusts droplet size per job without slowing the line.
For custom jobs with small barcodes or serial numbers, you need at least 600 dpi native resolution plus precise dot placement, otherwise scanners will struggle.
Yes, if the machine has a vacuum belt with adjustable tension and quick-drying ink sets, it can move from coated carton to matte film without stopping the queue.
Real-time preview, automatic job nesting, and support for CSV or XML input are essential, plus a logging system that records every printed record for traceability.
Not necessarily. Models with piezo printheads and waveform tuning maintain crisp characters and clean barcodes at speeds above 100 meters per minute.
Near-infrared or UV-LED curing depends on the ink, but the key is adjustable intensity zones so thin media doesn't warp and thick stock doesn't stay tacky.
Closed-loop spectrophotometers and nozzle-out detection with automatic compensation keep density stable, even when the data changes every print.
Automated printhead cleaning, quick-release ink manifolds, and self-aligning guides cut changeover time dramatically, especially for short run custom batches.
Conclusion
A factory floor running custom variable data jobs lives or dies by two things: whether the printhead can stay sharp after thousands of impressions, and whether the data pipeline chokes when it hits a million-record list. The best setups use printheads designed for continuous duty with precise droplet placement that doesn't drift as temperature and speed climb. They pair that with a RIP and data engine that pre-processes variable fields, so names, barcodes, and serial numbers stream through without stalling the press. Equally important is the drying path: gloss stocks, synthetic films, and heavy coated sheets each demand different airflow and heat profiles. A fixed dryer simply won't cut it when one job runs aqueous ink on matte paper and the next runs UV or solvent on polypropylene. Adjustable, zone-controlled drying heads keep output moving without smearing or curling.
Changeover speed matters more than most managers admit. If swapping from a 24-inch roll of uncoated paper to 350gsm coated board takes an hour of wrench work, short custom runs become unprofitable. Tool-free substrate changes—quick-release guides, auto-calibrating media sensors, and memory slots for repeat jobs—let operators switch between completely different stocks in minutes. That flexibility is only worth it when the press also catches its own mistakes. Inline vision systems that scan every piece, compare against the approved proof, and automatically reject flawed output before it reaches the shipping table save hours of manual sorting and prevent embarrassing client callbacks. Finally, modular stations for varnish, die-cutting, perforation, or additional color channels should be designed so one operator can set them up without a maintenance crew. If the modules take longer to configure than the run itself, they stop being a feature and become a bottleneck. A well-built variable data factory machine combines these elements so that custom work flows from file to finished piece with minimal intervention.
Contact Us
Contact Person: Jacky
Email: [email protected]
Tel/WhatsApp: 086 15000607053
Website: https://www.danmajet.com