Vulcanizing Press Factory Production Essentials for Reliable Rubber Molding
2026-09-01
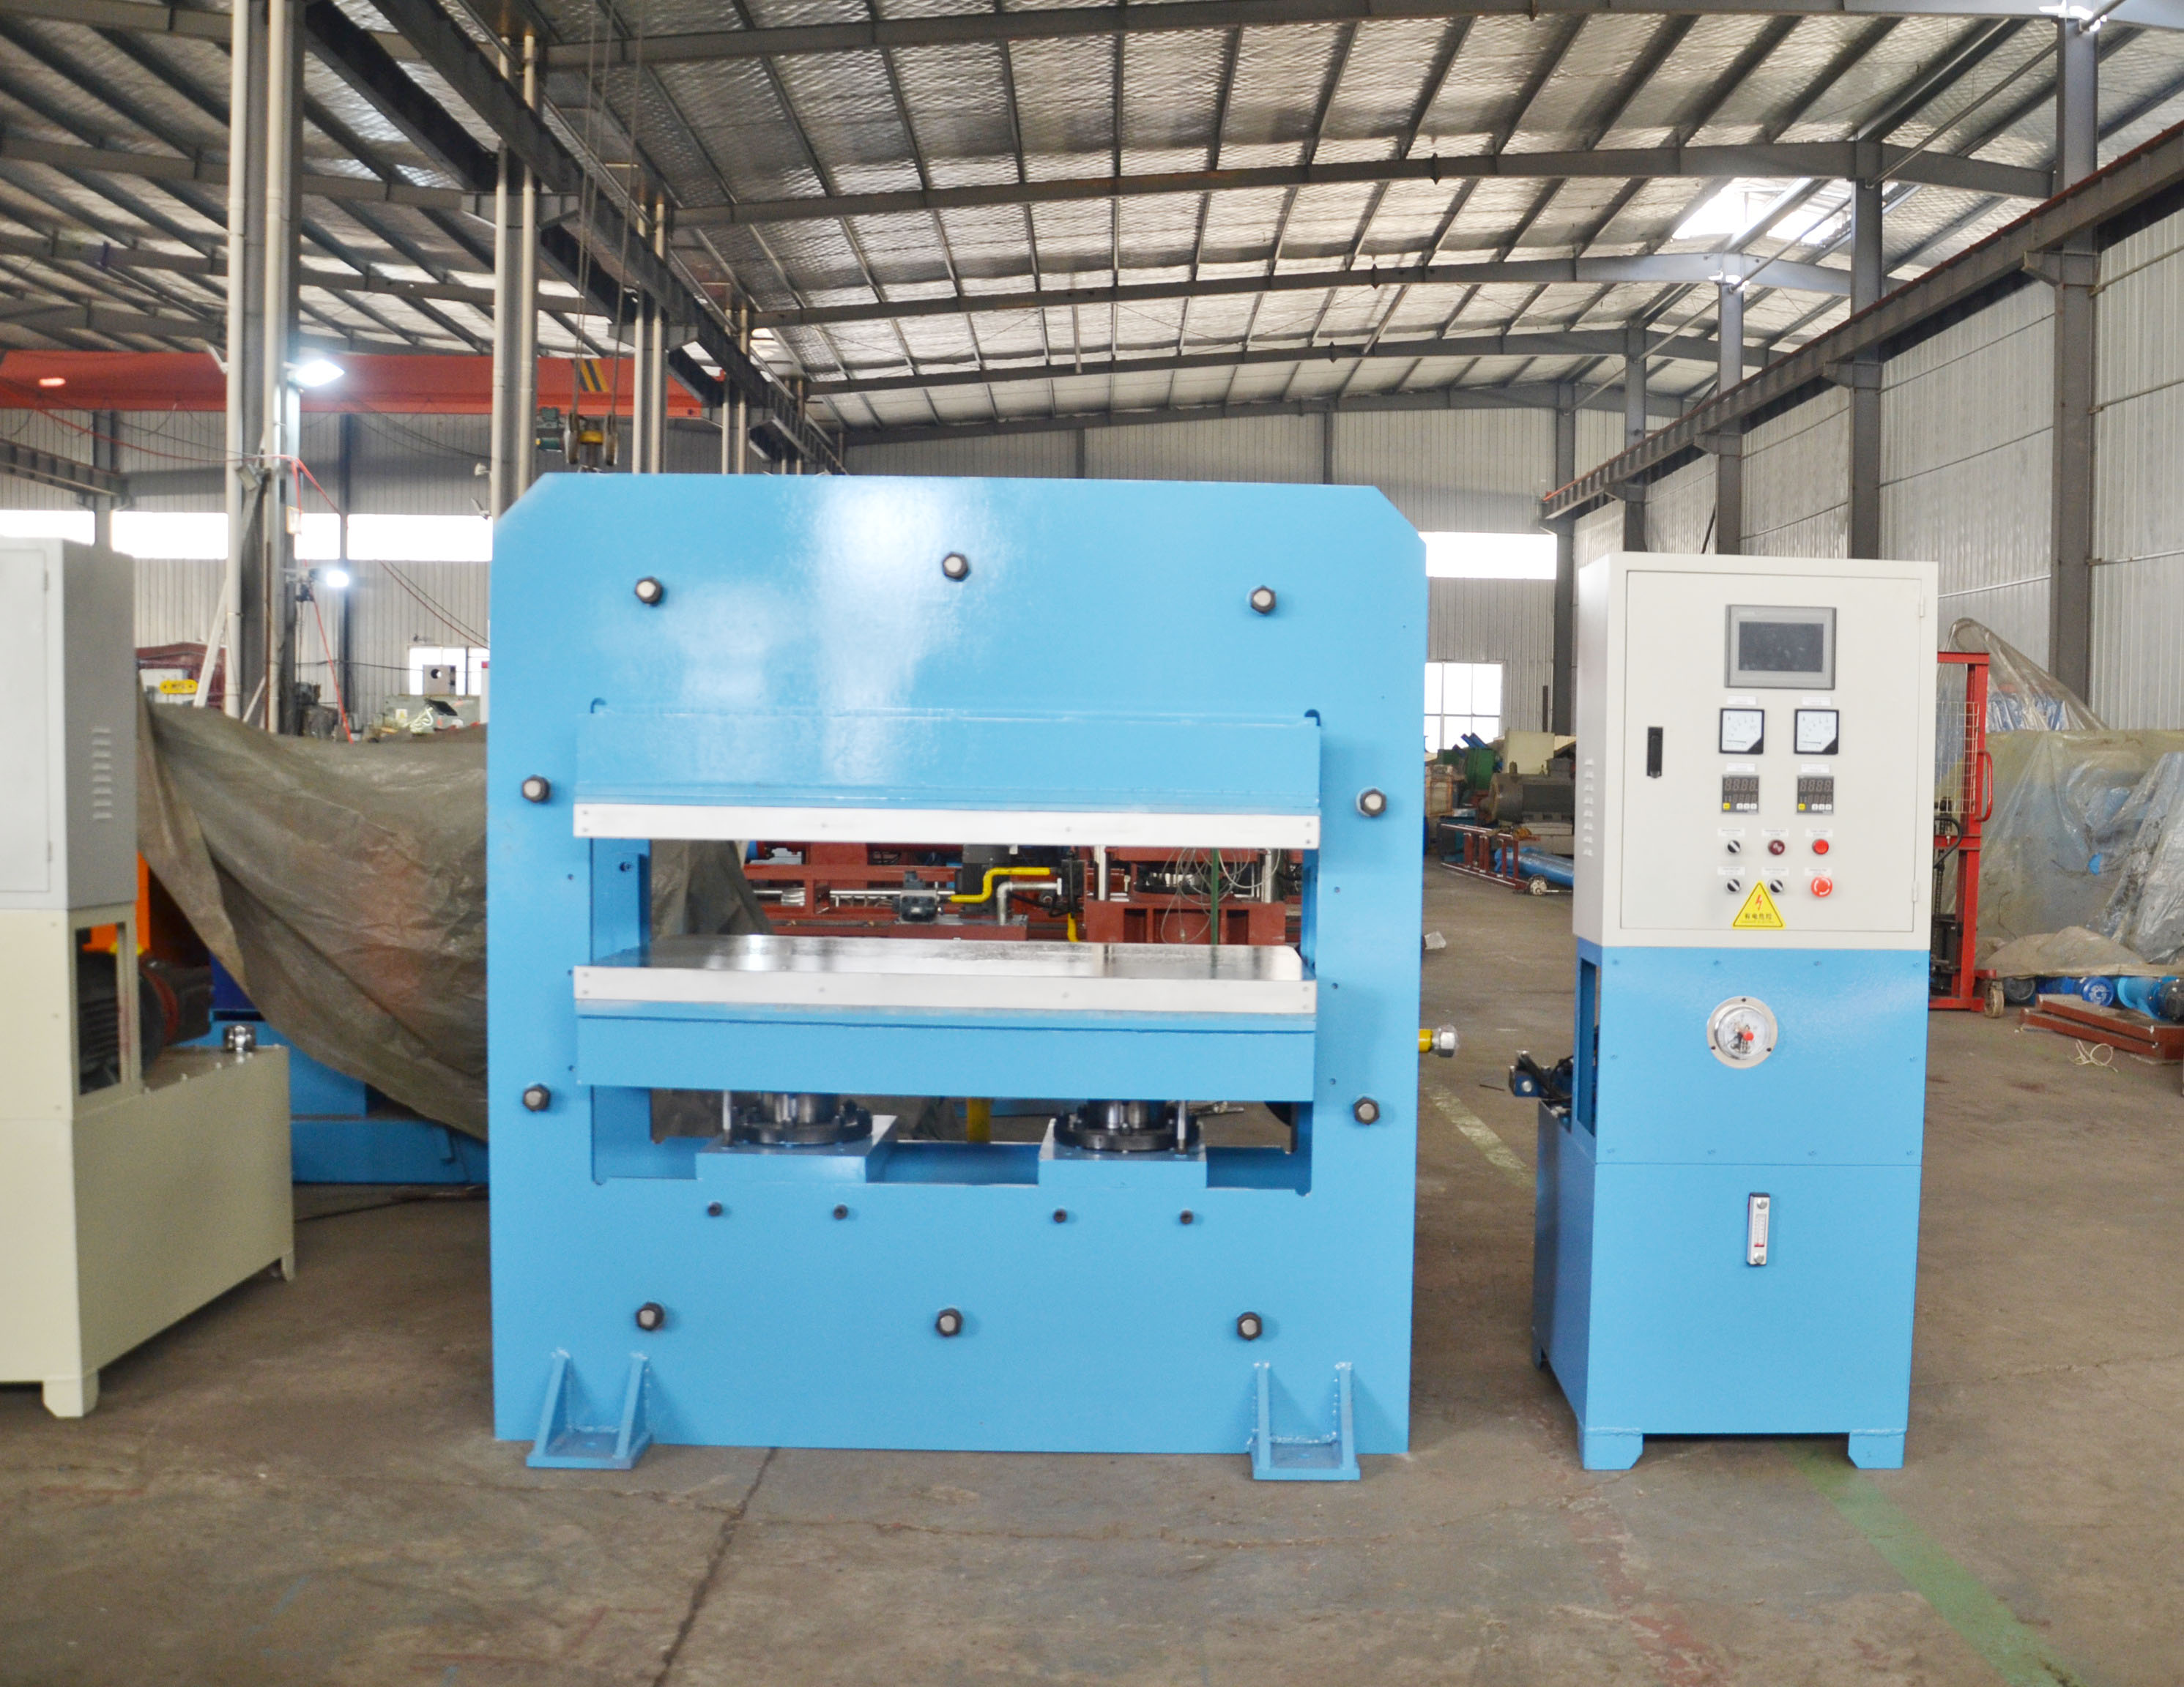
Ask any rubber molding engineer where quality is won or lost, and they’ll point to the vulcanizing press—not just the recipe. Getting reliable parts means controlling heat, pressure, and time across hundreds of cycles without drift. Yet many factories overlook the production basics that keep presses consistent. In this post, we strip away the guesswork and focus on practical essentials: from frame rigidity and platen parallelism to smart pre-heating and maintenance signals. Whether you're setting up a new line or troubleshooting uneven cure, these insights—drawn from SFC vulcanizing press engineering—will help you build a molding process that repeats the same way every shift.
Raw Compound Checks That Prevent Most Cure Defects
Most cure defects trace back to inconsistencies in the unvulcanized stock long before it ever reaches the press. Running a quick set of checks on the raw compound right after mixing gives you a chance to catch filler agglomerates, incorrect curative levels, and moisture pickup while the batch is still salvageable. These are not exotic tests—routine rheometer traces, Mooney viscosity readings, and specific gravity measurements reveal enough about batch-to-batch drift to stop problems at the source.
A practical screening sequence starts with scorch time and minimum viscosity from the rheometer. If scorch drops below the established window, it usually means the accelerator was double-charged or the mixing temperature ran too high. Density checks then flag over- or under-loaded fillers, while a simple hardness button press after a lab cure indicates whether the crosslink density will match production parts. For filled systems, a quick dispersion rating under a microscope catches undispersed carbon black or silica that would otherwise show up as surface blemishes or weak spots after vulcanization.
Tracking these numbers on a simple run chart turns the checks into an early warning system. A gradual rise in minimum torque across batches can signal progressive contamination or a worn mixer blade, even if each individual value stays within spec. Correcting the compound at this stage avoids the ripple effect of scrapped cured parts, mold cleaning cycles, and downtime. It also keeps the final product's appearance and dimensions consistent, which is far cheaper than chasing defects after the press opens.
Mold Venting and Runner Layout for Consistent Filling
Venting in injection molds often gets treated as an afterthought, yet it directly controls how air escapes ahead of the melt front. When vents are too shallow or poorly placed, trapped gas compresses, heats up, and burns the resin or creates short shots near the end of fill. A practical approach is to start with vent depths at the material's recommended safe limit—usually 0.02 to 0.05 mm for most thermoplastics—and then tune from there. You also need continuous venting along the parting line, not just a few isolated grooves, because air gets pushed into every corner of the cavity.
Runner layout works hand in hand with venting to keep the fill front uniform. If runners are unbalanced or too restrictive, some cavities fill early while others are still starved, leaving no place for air to escape except through the last cavity's vents. A naturally balanced runner system—where flow length and cross-section are identical to each cavity—reduces the need for aggressive vent adjustments. For multi-cavity molds, consider using full-round or trapezoidal runners with generous radii at turns; sharp corners create pressure drops that distort the melt front and trap gas pockets.
On the shop floor, consistent filling comes from observing the actual fill pattern rather than relying on simulation alone. Short shots run at incrementally higher injection pressures will show you exactly where the melt stalls and where vents choke. If you see burn marks or hesitation near the end of fill, widen the vent land or add a vent groove at that specific location. Sometimes moving the gate slightly or adjusting runner diameter does more for venting than adding more vent depth, because it changes how the air is pushed ahead of the polymer.
Platen Temperature Profiling Without the Guesswork
A press platen can read a steady 180°C on its controller while the actual working surface swings by 15 degrees from corner to corner. That’s the quiet failure mode most operators only discover when parts come out with inconsistent cure or bond strength. Profiling isn’t about chasing a single perfect number; it’s about capturing the thermal map your setpoint never shows you.
Run a profile with the platen closed against a dummy load, not just open to air. Use a grid of surface thermocouples or a thermal camera to track how heat spreads during ramp-up and how it sags once the press opens for part insertion. The data will often show a hot band near the heater elements and cooler edges that lag by minutes, not seconds. Adjusting zone offsets or adding insulation only makes sense after you’ve seen that pattern.
Repeat the profile after any change to heater wattage, platen thickness, or cycle timing. What worked on a small lab press rarely transfers directly to a production unit with larger thermal mass. A one-time profile is a snapshot; a series of them under real cycle conditions is what lets you set temperatures with confidence instead of habit.
Pressure Ramp Adjustments for Complex Part Geometries
When filling intricate cavities with sudden wall thickness shifts and deep ribs, a fixed pressure ramp often leaves hesitation marks or internal voids. Instead, map the flow front along the longest path first, then introduce a stepped ramp that holds lower pressure through narrow gates until the melt has wrapped around sharp corners. This prevents premature freezing at the edges while keeping shear rates below the point where material degradation starts.
For parts with uneven cross-sections, split the ramp into at least three segments: initial slow climb to seat the flow, a mid-fill plateau that lets thinner sections pack without overpacking adjacent thick bosses, and a final short spike only if the pressure drop across the last-to-fill region exceeds your sensor threshold. Run a short-shot series at each segment to confirm the transition points match actual fill, not just simulation predictions.
Cure Time Decisions Based on Real Batch Behavior
Waiting for a fixed cure window often ignores what each batch is actually telling you. By tracking real-time viscosity, exotherm, or hardness development on the line, you can release a batch only when its own curve says it is ready. Some mixes plateau early; others lag because of ambient shifts or slight ratio drift. Treating every batch as an individual signal rather than a calendar entry turns cure time from a guess into a measured decision.
The useful part is not just shortening average time, but catching the outliers before they cause rework. When a batch under-cures, downstream handling can smear, dent, or delaminate. When it over-cures, you waste energy and tie up molds or racks. Monitoring the actual batch lets you pull the trigger at the right hardness or conversion for your process, not for a lab ideal.
Operators tend to trust this approach more because it reflects what they see on the floor. Instead of a rule that says “bake for 40 minutes,” the decision becomes “bake until the temperature rise flattens and the surface reaches 70 Shore A.” That kind of guidance fits messy production reality, and it quietly improves consistency without adding paperwork.
Post-Press Handling to Lock In Final Dimensions
Once the ink has dried and the sheets leave the press, dimensional stability doesn't simply take care of itself. Paper remains sensitive to moisture, temperature, and mechanical stress well after printing. The way you handle the stock during cutting, folding, and binding can introduce subtle shifts that compound into misaligned layouts or uneven trim edges. A disciplined post-press environment—ideally with controlled humidity between 45% and 55% and stable temperatures—gives the fibers time to relax into a uniform state before any finishing operations.
Practical sequencing matters more than most teams realize. Letting printed sheets acclimate for 24 to 48 hours under the same conditions as the finishing area allows moisture gradients to equalize. Rushing straight from press to guillotine often locks in latent curl or waviness, which then transfer to the final product. For critical jobs, consider a two-stage trim: a rough cut to remove excess, followed by a rest period and a final cut to exact dimensions. This approach prevents the common problem of sheets shrinking slightly after the first trim, leaving you with undersized pieces.
Binding and folding choices also influence final size. Creasing before folding, for instance, reduces fiber cracking along the fold line and keeps the sheet's dimensions true. In perfect binding, a thin layer of adhesive can cause the spine area to swell slightly, so compensating the cover width by half a millimeter is often the difference between a crisp square back and a bowed edge. Small adjustments like these—based on test runs with the actual stock—lock in the dimensions you designed rather than the dimensions the production process happened to yield.
FAQ
Temperature uniformity across the platen, hydraulic pressure stability, and dwell time are the big three. Even a ten-degree drift or a few PSI of fluctuation can shift cure state enough to ruin a batch, so operators typically check these at set intervals rather than trusting automated readouts blindly.
Tonnage only provides clamping force; the mold dictates flow, venting, and heat transfer. A well-designed mold with balanced runner paths and proper vent channels can produce consistent parts on a modest press, while a poorly designed mold will create shorts, trapped air, and uneven cure no matter how large the machine is.
They keep the compound cool before it enters the cavity and use a press cycle that ramps temperature quickly only after the mold is closed. Some shops also pre-warm the stock to a lower, controlled temperature, which shortens flow time without triggering premature crosslinking at the gate.
Platen parallelism checks. People change hydraulic oil and inspect seals regularly, but if the platens are out of parallel by even a small amount, you get thickness variation and internal stress in molded parts. A simple dial indicator sweep every few weeks prevents a lot of hidden scrap.
Porosity, incomplete filling at thin sections, and poor knit lines usually point to low pressure or pressure drop during cure. Raising clamping force is only part of the fix; you often need to increase the injection or transfer pressure, adjust the preform shape, or reduce compound viscosity so the cavity packs fully before cure locks flow.
Use a higher temperature with a rebalanced cure system, but only after checking scorch safety and the thermal stability of the compound. Thinner preforms or preheated stock also help bring the part to cure temperature faster. The key is verifying tensile, compression set, and hardness on trial parts before changing production specs.
Two-hand trip or light curtain guarding, emergency stops at both operator positions, and lockout-tagout procedures during mold changes. Since the press works at high heat and pressure, operators also need thermal protective gloves and face shields when opening the mold, plus clear floor markings to keep bystanders away from the moving platen.
Rubber compounds age and can pick up moisture or lose accelerators if stored too long or too warm. Factories that keep raw stock in a cool, dry area with first-in-first-out rotation see far fewer variations in flow and cure behavior. Simple things like sealing partially used stock and recording the date on the pallet wrapper make a measurable difference.
Conclusion
Reliable rubber molding starts long before the press closes. A quick check of the raw compound's Mooney viscosity, scorch time, and dispersion quality catches most cure defects that later get blamed on the mold or the machine. Compound that sits too long or varies between batches will move differently in the cavity, so the mixing history matters. Once the material is right, mold venting and runner layout take over. Shallow vents at the last-fill points let trapped air escape without flash, while balanced runners keep every cavity seeing the same pressure at the same moment. Without this, even a perfect temperature profile will not fix short shots or porosity.
Platen temperature mapping is often skipped, but surface probes across the platen usually show a wider spread than the controller indicates. A quick profiling routine with a thermal camera or contact thermocouples gives a real picture, allowing the operator to offset zones and avoid undercured edges or overcured centers. For complex part geometries, a single pressure ramp rarely works. Stepping the clamp force up in two or three stages after initial flow lets the rubber fill thin ribs and deep bosses without trapping air. Cure time should not be locked to the original datasheet; it belongs to the actual batch. Checking a rheometer curve for each new lot, or cutting a sample from the first press cycle, shows when the state of cure is truly complete. After demolding, the part is still moving. Holding critical dimensions in a cooling fixture or supporting the part through a controlled cool-down prevents warpage and locks in final tolerances. These shop-floor habits together make press production predictable, not lucky.
Contact Us
Contact Person: Chen Zhengwei
Email: [email protected]
Tel/WhatsApp: +86-13963975727
Website: https://www.sfcrubbermachine.com